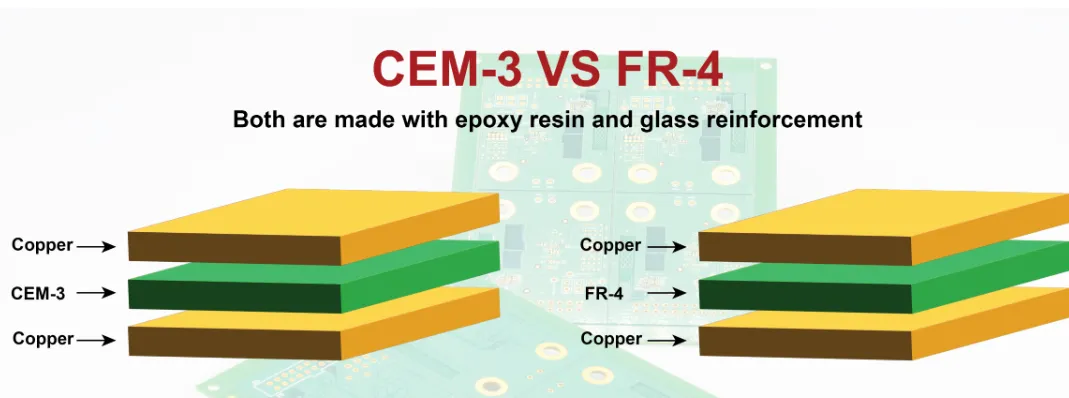
The FR4 vs high CTI FR4 decision is a surface-tracking and creepage decision, not a "stronger FR4" decision. Both laminates are glass-epoxy FR4. Drill, press, and etch stay on the same line. What changes is the resin-and-filler package that sets Comparative Tracking Index (CTI) under IEC 60112, and therefore which IEC 60664-1 material group the board is allowed to claim. Standard FR4 is the better manufacturing choice when working voltage is modest, pollution degree is 1-2, the layout already has the millimeters that Group IIIa demands, and unit cost plus stock availability matter more than a shorter creepage table. A high CTI FR4 PCB is the better choice when the safety file, compact layout, outdoor or dusty environment, or mains/high-voltage isolation distances only close if the laminate sits in Group II (CTI 400) or Group I (CTI 600).
From a fabrication standpoint, "FR4, UL94 V-0" does not buy you CTI 600. Most catalog FR4 lands around CTI 175-250 — Material Group IIIa. If the drawing never names CTI, CAM will buy that grade. We normally recommend writing the CTI floor, the material group you designed to, pollution degree, and working voltage as separate notes. High-CTI and high-Tg are independent knobs. Paying for one does not give you the other.
What Changes Between Standard FR4 and High-CTI FR4 on One Sheet
| Factor | Standard FR4 | High-CTI FR4 |
|---|---|---|
| Typical CTI (IEC 60112) | ~175-250 V (some mid grades to ~400) | Named 400 V or ≥600 V on the slash sheet |
| IEC 60664-1 material group | Usually IIIa (175-400) | II (400-599) or I (≥600) |
| UL PLC (typical) | PLC 3 (175-249) common | PLC 1 (400-599) or PLC 0 (≥600) |
| Tracking resistance | Baseline; carbon path forms sooner under contaminant + voltage | Resin/filler package resists surface carbonization |
| Creepage (same V, PD 2) | Longest table values in Group III | Shorter allowed path in Group II / I |
| Clearance (air) | Set by voltage, altitude, overvoltage category | Same air rules; CTI does not shrink clearance |
| Tg / Td / process | Full Tg catalog; default recipes | Still FR4 process; confirm Tg separately |
| Manufacturing complexity | Widest window, every shop | Same line; stock and UL file must match the grade |
| Laminate / board cost | Baseline | Typically +10-25% laminate; finished board often +5-15% |
| Availability | Stocked almost everywhere | Common CTI 600 cores in Asia power lines; odd thickness adds days |
| Typical applications | Low-voltage digital, indoor consumer with generous spacing | SMPS, EV / charger, industrial drives, appliance mains, outdoor HV |
Which Grade Wins When the Priority Changes
| If your priority is... | Better choice | Why factories lean that way |
|---|---|---|
| Lowest unit cost, low voltage | Standard FR4 | Default stock; CTI 600 adds nothing if Group IIIa already fits |
| Safety file written to Group I | High-CTI FR4 (CTI ≥600) | Standard FR4 cannot be tested into Group I |
| Shorter creepage on a tight outline | High-CTI FR4 | Material group is what the creepage table uses |
| Fast prototype at any shop | Standard FR4 | High-CTI cores are not on every shelf |
| Lead-free multilayer thermal reliability | Match Tg, then CTI | High-CTI is not high-Tg; specify both if both matter |
| Pollution degree 3 / outdoor dust | High-CTI FR4 | Tracking risk is a surface-contaminant problem |
| Hipot only, generous spacing | Standard FR4 | Hipot is bulk dielectric; CTI is a different failure mode |
What CTI Actually Measures — and What It Does Not
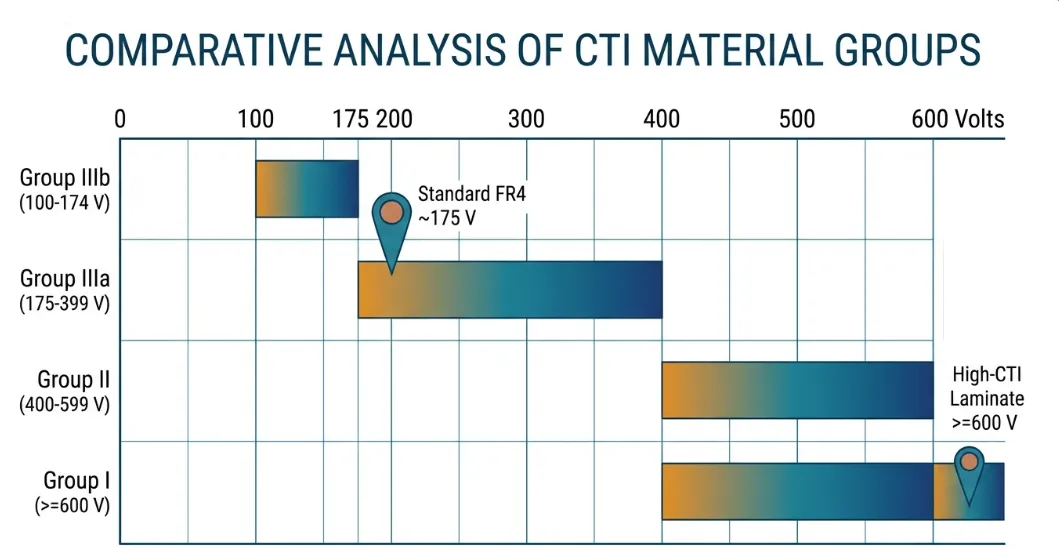
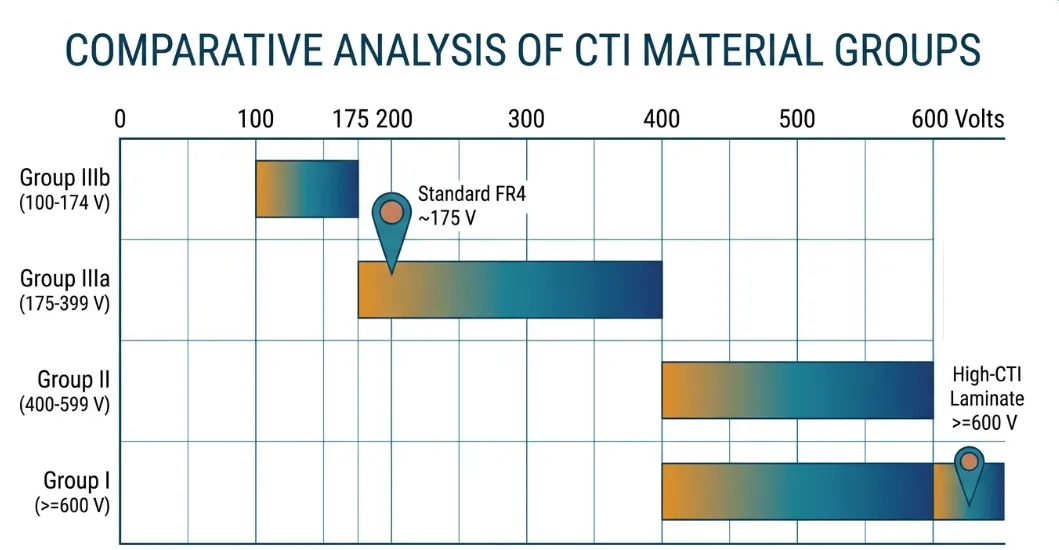
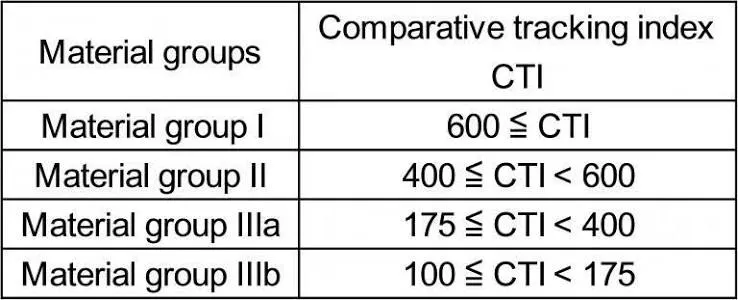
CTI is the voltage at which a material survives a defined electrolyte-drop tracking test (IEC 60112) without forming a conductive carbon path. The number is reported in volts. Safety standards then bucket that number into material groups: Group I at CTI ≥600, Group II at 400-599, Group IIIa at 175-399, Group IIIb at 100-174. UL uses Performance Level Categories that map the same ranges (PLC 0 at ≥600, PLC 1 at 400-599, PLC 3 at 175-249, and so on). During CAM review, those buckets are the only language that matters. A datasheet that says "good tracking resistance" without a CTI and a method is not a spec.
Standard FR4 is not a poor insulator in the bulk. Dielectric strength through the thickness is still in the usual FR4 band. Hipot between layers can pass on CTI 175 material. Tracking is a surface event: voltage + moisture + ionic contamination + time. That is why a high CTI FR4 PCB is specified for high-voltage work that lives in the real world, not for a clean lab hipot. Proof Tracking Index (PTI) is the related pass/fail check at a stated voltage; do not mix PTI 250 with a CTI 600 claim.
Two other numbers get dragged into this FR4 vs high CTI FR4 comparison and do not replace CTI. Tg tells you when the resin softens. Td and T288 tell you how the book survives lead-free heat. None of them move the creepage table. We normally ask for CTI, Tg, and UL94 as three separate lines.
Why Creepage Shrinks on High-CTI FR4 and Clearance Does Not
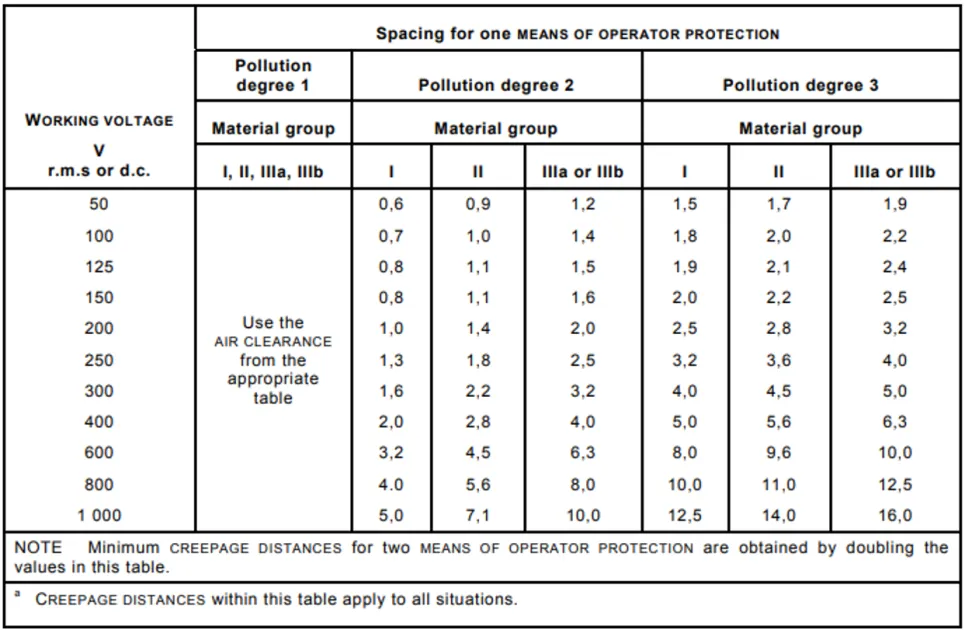
Clearance is the shortest path through air. It follows working voltage, overvoltage category, and altitude. The laminate group barely enters that conversation. Creepage is the shortest path along the insulating surface. IEC 60664-1 (and product standards that point to it, including many appliance and power-supply files) sets creepage from working voltage, pollution degree, and material group. Group IIIa on standard FR4 takes the long column. Group I on a CTI 600 grade takes the short column. On a 400 V RMS, pollution degree 2 example, that is the difference between roughly 4 mm and 2 mm of basic-insulation creepage in the commonly cited table subset — not a rounding error on a compact converter.
That is the manufacturing reason high-CTI exists. The designer wants the same isolation rating on a smaller outline. The factory can only honor that layout if the laminate group on the incoming sheet matches the group used in the calculation. If you designed 2.0 mm primary-to-secondary creepage assuming Group I and we build standard FR4, the board can still etch, plate, and pass hipot. The safety spacing you thought you bought is not there.
Slots, ribs, and soldermask do not erase the laminate callout. A milled slot converts a surface path into a mix of air and remaining laminate edge; it is a layout tool, not a substitute for naming CTI. Soldermask CTI is its own number. A high-CTI core under a low-CTI mask still presents a tracking surface where the mask is thin, damaged, or missing at the pad. We normally treat soldermask and laminate CTI as two items on the same high-voltage drawing.
Where High-Voltage Products Actually Force the Upgrade
In production, the upgrade from standard FR4 to a high CTI FR4 PCB shows up on offline SMPS primary-secondary barriers, PFC stages, industrial drives, EV onboard chargers and DC-DC boards, PV inverters, appliance mains controllers, and outdoor lighting or meter boards that see condensation. Those files already name working voltage and often name pollution degree. Once the mechanical envelope is tight, Group IIIa spacing no longer fits and the material note has to move.
Indoor low-voltage digital, 12-48 V industrial I/O with wide pour gaps, and consumer boards that never see mains on the same laminate usually stay on standard FR4. Adding CTI 600 there is a cost adder with no safety-file return. The trade-off is the opposite on a 85-265 VAC input board that was laid out to Group I distances: standard FR4 is the cheaper sheet and the wrong sheet.
Pollution degree is the other switch. Degree 2 (normal indoor, non-conductive dust, occasional condensation) is where most electronics live and where Group I vs IIIa already moves millimeters. Degree 3 (conductive pollution or expected condensation) makes tracking more likely and makes the high-CTI call easier to defend. Degree 1 clean, sealed assemblies can sometimes stay on standard FR4 even at higher voltage if clearance and creepage were sized for Group III from the start. Do not assume sealed equals Group I.
Cost, Stock, and Why the Process Window Barely Moves
High-CTI FR4 is still FR4 on the floor. Drill feeds, desmear, oxide, and press cycles stay in the FR4 family. Yield on a qualified grade is comparable to standard FR4 of the same Tg and thickness. The factory differences are incoming identification, UL / IEC file coverage, and whether the core and prepreg family is on the rack. Mix a CTI 175 inner with a CTI 600 outer and the book is no longer the group you declared.
Cost is real but not dramatic. Laminate is typically 10-25% above the equivalent standard-Tg FR4 sheet. Finished-board adders often land around 5-15% on a 2-layer or 4-layer power board when the shop already runs that grade. Odd thicknesses, locked brands, and combining high-CTI with halogen-free plus high-Tg stack the adder. Prototype houses that do not stock CTI 600 will either substitute silently — which we refuse on a named CTI note — or add lead time to buy the sheet.
Availability follows the power-supply market. CTI 600, 1.0-1.6 mm, 1 oz constructions are common in Asia on lighting and PSU lines. Thin cores, heavy copper, and high-Tg high-CTI combinations are less universal. If the RFQ is "any FR4, five days," you will get Group IIIa. If the RFQ names CTI ≥600 and a slash sheet, the quote clock starts at material check, not at CAM.
How CAM and DFM Treat a High-Voltage Material Note
During DFM we look for four things that are often missing on FR4 vs high CTI FR4 RFQs. One: a numeric CTI or material group, not the words "high voltage FR4." Two: whether inner cores and prepregs are included — a high-CTI face sheet over standard prepreg is a documentation fight later. Three: soldermask type if the safety lab will ask for the assembled surface. Four: Tg and CTI written apart, so nobody "covers" a 170°C need with a CTI 600 sheet that is still Tg 135.
CAM does not re-calculate creepage. If the Gerber shows 2.2 mm primary-to-secondary and the note says CTI 175, we will not stop the job for spacing unless the customer asked for a high-voltage design review. That gap is how lots ship that pass electrical test and fail the first safety audit. We normally recommend a spacing plot or a marked isolation drawing when the board is a reinforced-insulation part.
Inspection does not change much: same AOI, same hipot if specified. First-article paperwork should include the laminate slash sheet and CTI statement, not just "FR4." Tooling is unchanged. Panel utilization is unchanged. Process risk is substitution and mixed lots. Shops that run both grades keep them on separate racks and check the manufacturer mark before lay-up. What factories usually recommend: stay on standard FR4 when the layout was sized for Group III and the file is silent on CTI. Move to a named high CTI FR4 PCB when the creepage table, the AVL, or the notified-body report already assumes Group II or Group I.
Which Material Note You Should Release
Choose standard FR4 if you:
- Are below mains or have already drawn Group IIIa creepage with margin
- Need any-shop prototype speed and default stock
- Have a hipot spec but no tracking or material-group requirement
- Would rather spend millimeters of board than a laminate adder
- Have not named CTI, pollution degree, or a safety standard that uses material groups
Choose high-CTI FR4 if you:
- Designed creepage to Material Group I or II and need the laminate to match
- Are building SMPS, EV / charger, industrial drive, appliance mains, or outdoor HV boards
- Face pollution degree 2-3, condensation, or conductive dust on the surface
- Need a shorter isolation path to keep the outline or transformer span legal
- Can name CTI ≥400 or CTI ≥600, the matching prepreg family, and Tg as separate lines
There is no universal winner in this FR4 vs high CTI FR4 comparison. Standard FR4 still wins on cost, availability, and process familiarity when the spacing already assumes Group IIIa. A high CTI FR4 PCB wins the moment the safety table or the layout only works on Group II or Group I. Tracking resistance is the reason to pay. Tg, hipot, and "high voltage" printed in a title block are not substitutes for a CTI number.
Questions Buyers Ask Before They Lock the CTI Line
Q1: What CTI does standard FR4 actually have?
A1: Most commodity FR4 sits around CTI 175-250 V (Material Group IIIa / UL PLC 3). Some mid grades reach the 250-400 band. None of that is CTI 600 unless the slash sheet says so. Read the datasheet; do not infer CTI from Tg or UL94 V-0.
Q2: Does high-CTI FR4 let me cut clearance as well as creepage?
A2: No. Clearance is an air-gap rule. CTI only changes the material group used for creepage along the surface. If the limiting path is through air or through a slot, high-CTI will not shrink it.
Q3: Is high-CTI the same as high-Tg or halogen-free FR4?
A3: No. You can buy Tg 130 with CTI 600 and Tg 180 with CTI 175. Halogen-free is a third axis. Write CTI, Tg, and halogen limit as separate requirements so the shop does not satisfy one and miss the others.
Q4: How much extra does a high CTI FR4 PCB cost?
A4: Plan on roughly 10-25% more for the laminate and about 5-15% on a typical finished power board if the grade is already stocked. Locked brands, odd cores, and stacking high-CTI with high-Tg or halogen-free cost more than a shop's standard CTI 600 equivalent.
Q5: Will soldermask or a slot replace a high-CTI laminate?
A5: Not as a spec substitute. Slots change the path geometry. Soldermask has its own CTI and can be damaged at pad edges. If the safety calculation used Group I laminate, the incoming sheet still has to be Group I.
Q6: What should the fabrication drawing say so the factory does not ship standard FR4?
A6: State "FR4, CTI ≥600 per IEC 60112 (Material Group I)" or CTI ≥400 if that is what you designed, plus Tg, UL94 V-0, and "cores and prepreg same family — standard FR4 not acceptable." Name the slash sheet if substitution is forbidden. A note that only says "high voltage FR4" is how Group IIIa material lands on a Group I layout.