Flexible PCB prototyping is an important step between the initial circuit design and full-scale production. A functional flexible PCB prototype allows engineers to check electrical performance, mechanical flexibility, connector fit, assembly compatibility, and overall product integration before committing to mass production.
Compared with rigid PCBs, flexible circuits require additional attention to material selection, copper structure, bend areas, coverlay, reinforcement, and manufacturing tolerances. A design that works in a prototype may still need further adjustment before it can be produced consistently at higher volumes.
Highlights
• Prototype shops optimize for speed and design flexibility; volume fabs optimize for repeatability, statistical process control, and cost.
• Early formal DFM with the production fabricator, correct tooling decisions, and pilot-run validation prevent most scaling failures.
• Material standardization, panel nesting efficiency, and shared cost/lead-time planning with the supplier deliver the largest gains in both unit cost and schedule.
This guide explains the key considerations involved in flex PCB prototyping, including design review, material selection, fabrication, testing, DFM, and the transition from an FPC prototype to mass production.
What Is Flexible PCB Prototyping?
Understanding a Flexible PCB Prototype
Flexible PCB prototyping is the process of producing a small number of flexible printed circuit boards to evaluate a design before volume manufacturing. A flexible PCB prototype is normally used to verify whether the circuit meets the required electrical, mechanical, and assembly requirements.
Depending on the application, a prototype may be used to check:
-
Circuit functionality and signal continuity
-
Component placement and solderability
-
Connector and ZIF fit
-
Bend performance and installation clearance
-
Layer alignment and mechanical dimensions
-
Compatibility with the final product housing
-
Manufacturing feasibility and potential design risks
The purpose of a flex circuit prototype is not only to confirm that the circuit works. It also helps identify issues that may affect reliability, cost, or production efficiency later.
Why FPC Prototyping and Mass Production Are Fundamentally Different
Prototype runs exist to prove electrical function, mechanical fit, and basic reliability. The fabricator accepts material substitutions, manual stiffener attachment, flying-probe testing, and laser or soft-tool outline cutting because speed and design change tolerance matter more than unit cost. Mass production demands a stable process window, lot-to-lot material traceability, high panel utilization, automated stiffener placement, bed-of-nails or fixture testing, and hard tooling so that every board leaving the line meets the same dimensional and reliability targets.

The root causes of the gap are simple. Prototype shops are organized around rapid CAM, flexible process recipes, and low fixed overhead. Volume fabs invest in SPC, dedicated fixtures, and process parameters tuned for thousands of cycles. Material behavior that is invisible at low volume becomes visible at scale: Prototype-to-production scaling often exposes dimensional changes caused by moisture conditioning, lamination, thermal cycling, and material mismatch; adhesive flow under repeated lamination pressure creates squeeze-out or voids; coverlay registration tolerance that was acceptable on a laser-cut panel fails when a steel-rule die or progressive tool is used.
Common failure modes that appear only at volume include adhesive squeeze-out under stiffeners, coverlay voids at pad edges, progressive dimensional drift after reflow, and flex-to-install cracking caused by residual stress from unbalanced copper or asymmetric coverlay. These are not random defects—they are the predictable result of treating a production process as a larger version of the prototype process.
FPC DFM Checklist Before Moving Into Production
DFM is the highest-leverage activity before tool release. A formal review with the chosen production fabricator, ideally before the design is frozen, catches the issues that later become expensive respins. Organize the review around these practical groups.
Stack-up and material selection
Specify consistent polyimide thickness across lots, choose acrylic or epoxy adhesive deliberately, and select RA copper for dynamic flex or ED copper only when cost and static applications allow. FPC coverlay versus flexible soldermask must be decided early, since coverlay remains the reliability standard for dynamic or high-temperature use, while soldermask can reduce cost on static consumer parts. At volume, lot-to-lot material variation that was tolerable in prototypes drives yield loss and impedance drift.
Material selection directly affects the performance and manufacturability of a flexible PCB prototype. Common material considerations include the flexible dielectric, copper foil, coverlay, adhesive system, stiffeners, and shielding materials.

Dimensional and tolerance rules
Minimum FPC bend radius must be set relative to finished thickness. Coverlay opening-to-pad clearance, stiffener-to-pad registration, and overall length/width tolerances must include the fabricator's measured material shrinkage factors. Ignoring shrinkage produces parts that no longer fit the mechanical housing after multiple thermal cycles.
Panelization and tooling design
Panel layout and tooling features must work together so the boards can move smoothly through automated assembly. Break-tab strength needs to hold the array together during processing yet separate cleanly without tearing the flexible PCB material. The choice between routing and punching depends on volume and outline complexity. Laser or soft tooling is fine for low quantities, while punching dies become the practical option once volumes rise and edge consistency matters.
Fiducials and tooling holes must be positioned so assembly equipment can locate the panel accurately every time. Prototype panels usually keep generous borders and lower density because speed and design changes matter more. Production panels aim for higher material utilization while still providing the mechanical stability and correct tooling features needed for SMT carriers. Poor nesting wastes material and can easily double the unit cost, even when the circuit design itself is sound.
Stiffener and mechanical features
FR4, polyimide, or stainless-steel stiffeners require defined attachment methods. PSA for prototypes, thermal-bond or thermosetting adhesive for volume. Selective windows and keep-out zones near bend areas must be documented. Manual attachment that works for 20 pieces becomes a bottleneck and a source of registration error at 5,000 pieces.

Electrical and reliability requirements
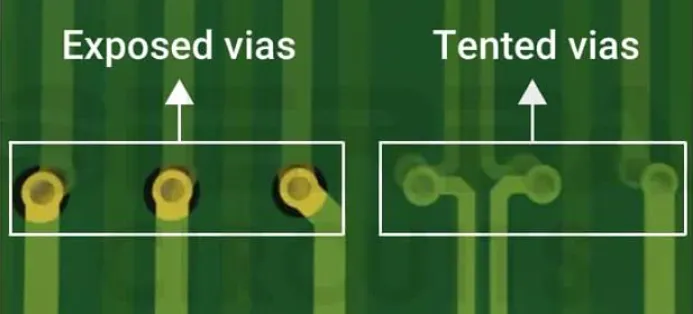
Controlled-impedance feasibility must be confirmed against the volume process window, not only the prototype stack-up. Via fill or tenting decisions affect both reliability and cost. Dynamic flex cycle life should be validated on production-intent materials and processes, not only on prototype coupons.
Testability and assembly
Probe-pad accessibility, component keep-out near bend areas, and the need for carrier panels or vacuum fixtures must be designed in. SMT on unsupported flex produces tombstoning and placement errors that flying-probe testing will never catch.

|
DFM Area |
What to Review |
Production Risk |
|---|---|---|
|
Stack-up & Materials |
PI, copper, adhesive, coverlay |
Yield and impedance variation |
|
Dimensions & Tolerances |
Shrinkage, registration, bend radius |
Fit and registration failures |
|
Panelization |
Nesting, tooling holes, fiducials |
Higher unit cost |
|
Stiffeners |
Material, adhesive, placement |
Bonding and registration issues |
|
Reliability |
Flex cycles, thermal cycling |
Field failures |
|
Assembly & Test |
Carriers, probe access, fixtures |
Placement and test defects |
How Materials and Process Windows Change at Production Volume
Polyimide absorbs moisture and exhibits higher CTE than copper. In short prototype cycles the effect is small; in continuous volume lamination the cumulative dimensional change requires artwork scaling and tighter incoming material control. RA copper provides superior flex life but etches differently from ED copper, so etch uniformity and surface treatment must be locked. Coverlay remains preferred for most dynamic and high-reliability applications; flexible soldermask can be cost-effective only when the application is purely static and the volume justifies the process qualification.
Flex PCB Tooling and Fixture Strategy for Volume Production
Prototypes rely on laser cutting or low-cost steel-rule dies. Volume production almost often requires additional tools: outline dies, coverlay cutting dies, stiffener punching dies, custom test fixtures, and carrier panels or vacuum fixtures for automated SMT.

For pilot runs and designs that are still evolving, soft tooling, such as laser cutting or simple steel-rule dies, is usually enough. Hard tooling only becomes necessary when yearly volume is high enough to recover the investment, when outline tolerances are tight, or when cleaner edges and faster cycle times are required. Steel-rule dies can typically be ready in a few days to two weeks. Hard progressive dies take longer, often several weeks, and cost more, but once in place they deliver the consistency and throughput that sustained production needs.
Once hard tooling is cut, design changes become expensive. That is why critical dimensions must be frozen early. At the same time, clarify with the fabricator who owns the tools, where they will be stored, how they will be maintained, and what happens if production ever needs to move. In production, AIVON engineers evaluate carrier and fixture requirements together with the flexible PCBs panel design, particularly when thin flex circuits must enter SMT and reflow processes. The goal is to stabilize the panel before assembly rather than compensate for unsupported flex during placement. Thin flexible circuits simply will not stay flat and clean through SMT and reflow without them.
How to Reduce FPC Production Cost and Lead Time
Total cost at volume comprises material, process steps, yield loss, tooling amortization, testing, and logistics. The practical levers that reduce both cost and lead time without sacrificing reliability are:
● Standardize polyimide and copper constructions early and qualify dual sources.
● Improve panel utilization through collaborative nesting rather than accepting the prototype layout.
● Consolidate process steps, for example, combining certain stiffener and coverlay cycles, where process windows allow.
● Move from 100 % flying-probe testing to a mix of AOI plus sample or fixture electrical test once the process is stable.
● Plan safety stock for long-lead materials.
● Qualify a second-source fabricator in parallel so capacity or disruption risk is managed.
A realistic timeline from design freeze to first production lot for a medium-complexity flex printed circuit is typically 6 to 12 weeks, covering tooling, pilot builds, and qualification. At AIVON, standard prototype builds ship in 9 to 12 days, while volume production lots are typically completed in about 14 to 20 days once the process is fully set up.

Each DFM or tooling decision that is deferred lengthens the overall window; each one closed early shortens it. Avoid false economies. The cheapest material or lowest quoted unit price is not necessarily the lowest total cost if it later causes yield loss, delays, or field failures.
Common Problems During Flexible PCB Prototyping
The Prototype Works but Does Not Fit the Product
A flexible PCB prototype may pass electrical testing but fail during installation because of incorrect dimensions, connector position, bend direction, or interference with other components.
To reduce this risk, the prototype should be tested in a representative product assembly or fixture.
The Prototype and Production Board Have Different Results
Differences between prototype and production results may occur when the two stages use different materials, equipment, or process conditions.
The project team should confirm that the approved prototype specifications can be transferred to the intended production process.
The Flexible Circuit Is Too Thick in the Bend Area
A flexible circuit may become difficult to bend when several layers, stiffeners, components, or protective materials overlap in the same area.
The design should review the total local thickness rather than considering only the flexible base material.
The Prototype Has Unexpected Manufacturing Costs
Prototype costs may increase because of small quantities, special materials, complex tooling, manual processing, or low production efficiency.
A DFM review can help identify opportunities to simplify the design and prepare it for higher-volume flex PCB manufacturing.
The Prototype Does Not Reflect the Final Application
A prototype may not provide useful results if it does not reproduce the final bend condition, connector, housing, assembly method, or operating environment.
The prototype plan should therefore include the key mechanical and electrical conditions expected in the final product.
Testing Is Insufficient Before Mass Production
Moving directly from a first working prototype to mass production may leave mechanical, assembly, or reliability issues undiscovered.
A staged validation process helps confirm that the design is ready for the intended operating and manufacturing conditions.
FPC Production Readiness Checklist
Use these gates as a go/no-go scorecard:
1. Formal DFM review with the production fabricator is complete and closed.
2. All critical tolerances, materials, and stack-up details are frozen.
3. Tooling strategy and ownership are agreed in writing.
4. First-article and reliability qualification plan is defined.
5. Yield target and cost model are accepted by both engineering and procurement.

Run a pilot of appropriate size against the success criteria before full ramp. Late design changes should be evaluated against tooling impact and schedule; minor ECOs can sometimes be absorbed, but major changes usually require new tools or process re-qualification.
How AIVON Supports FPC Prototype-to-Production Scaling
In one recent project, a customer submitted a panel layout designed with rigid-board rules. After the first prototype run, the flexible boards broke frequently during handling and depanelization because the connecting tabs were too weak and the process borders were insufficient.
AIVON's engineering team reviewed the panel design as part of the standard DFM process for production readiness. We recommended adding 3 mm process borders on both the left and right sides of the panel so that stronger connecting tabs could be placed on both sides. The revised panel maintained good material utilization while providing the mechanical stability needed for automated handling and SMT carriers.
After the updated panel was implemented, breakage during processing disappeared and assembly yield improved.This type of early, detailed feedback is typical of how AIVON works with customers throughout the prototype-to-production journey. From the first design review, our engineers focus on identifying issues that only become critical at volume, such as panelization strength, tooling feasibility, material consistency, and assembly handling. We treat the prototype stage as the starting point for production process definition, not a separate activity. This approach helps customers avoid unexpected yield drops, dimensional problems, and schedule delays when quantities increase, while keeping communication clear and technical decisions practical.
Conclusion
Flexible PCB prototyping helps engineers validate a flexible circuit before investing in mass production. In addition to electrical functionality, the prototype should be evaluated for mechanical fit, bend performance, connector compatibility, material selection, coverlay structure, and manufacturing feasibility.
A successful transition from a flexible PCB prototype to mass production requires more than confirming that the first sample works. DFM review, material confirmation, process validation, testing, and production planning are all important parts of the process.
By working with an experienced flex PCB manufacturer, companies can identify potential issues earlier and improve the consistency of the final product. A structured approach to flex PCB prototyping can support better design decisions, smoother production transfer, and more reliable flexible circuits.
FAQs
Q1: How early should hard tooling be ordered for flexible PCB volume production?
A1: Hard tooling should be ordered only after the design is frozen and the pilot build has been successfully validated. Soft tooling or laser processing is generally more suitable during the prototype and pilot stages. Because hard tooling can require several weeks to manufacture, the order should be placed early enough to ensure the tools are ready before the first production lot is scheduled.
Q2: Which DFM rules are most commonly missed on flexible circuits?
A2: Commonly missed DFM requirements include insufficient bend-radius margins relative to finished thickness, coverlay opening-to-pad clearances that do not account for registration tolerance, unbalanced copper or asymmetric coverlay that can cause warpage, and missing or poorly positioned fiducials and tooling holes for automated assembly.
Q3: Can the same polyimide material used in prototypes be used for mass production without requalification?
A3: Only when the same material grade, thickness, copper type, and adhesive system are maintained using the same or dual-qualified suppliers, and the volume manufacturing process window has been validated. Material lot-to-lot variation that is not apparent during prototyping can affect dimensional stability, impedance, and overall production consistency at scale.
Q4: How do stiffener attachment methods change between prototype and volume FPC runs?
A4: Prototypes commonly use pressure-sensitive adhesives and manual stiffener placement for flexibility during development. Volume production typically uses thermosetting or thermal-bond adhesives with automated or semi-automated placement under controlled heat and pressure. This improves registration accuracy, process consistency, and long-term bond strength.
Q5: What is the purpose of a flexible PCB prototype?
A5: A flexible PCB prototype is used to verify a circuit's electrical performance, mechanical fit, bend behavior, connector compatibility, and assembly requirements before mass production. It helps identify design and manufacturing issues while changes are still relatively easy to make.
Q6: How long does flexible PCB prototyping take?
A6: The time required for flexible PCB prototyping depends on the layer count, material system, circuit complexity, tooling, testing requirements, and order quantity. At AIVON, flexible PCB prototypes typically take around 9–12 days, although the actual lead time may vary depending on the design and manufacturing requirements. Simple designs may require less time, while multilayer, fine-line, rigid-flex, or specially reinforced circuits may need additional engineering and fabrication time.
Q7: What files are needed for a flex PCB prototype?
A7: A manufacturer will normally need Gerber files, drill files when applicable, a fabrication drawing, stackup information, material requirements, board dimensions, bend specifications, and assembly information if components are included. Connector details, stiffener requirements, and testing expectations should also be provided when relevant.
Q8: Can a flexible PCB prototype be used for mass production?
A8: A prototype can provide a foundation for mass production, but it may require further DFM review and process validation. The manufacturer should confirm that the prototype materials, stackup, tolerances, and fabrication methods can be transferred to the expected production process.
Q9: What is the difference between a flex PCB prototype and a production board?
A9: A flex PCB prototype is usually produced in a smaller quantity to validate the design. A production board is manufactured using a controlled process designed for repeatability, yield, quality consistency, and the required production volume. The design may remain similar, but the manufacturing process and inspection requirements may be more extensive.
Q10: What should I check during flexible circuit prototyping?
A10: During flexible circuit prototyping, check electrical performance, board dimensions, bend areas, connector fit, component clearance, coverlay alignment, stiffener placement, assembly compatibility, and any application-specific testing requirements.
Q11: Why should DFM be reviewed before flex PCB mass production?
A11: DFM review helps identify design features that may cause manufacturing difficulties, low yield, additional cost, or inconsistent quality. It is especially useful when moving from flex PCB prototyping to mass production because prototype-friendly features may not always be suitable for high-volume manufacturing.
Q12: How do I choose a manufacturer for flexible PCB prototyping?
A12: Look for a manufacturer with experience in flexible PCB materials, multilayer circuits, coverlay, stiffeners, connectors, electrical testing, DFM review, and production transfer. It is also useful to confirm whether the supplier can support both the flexible PCB prototype stage and future mass production.
Q13: Can the same flexible PCB manufacturer handle prototypes and mass production?
A13: Many manufacturers can support both stages, but their capabilities should be reviewed before placing an order. Ask about prototype fabrication, material availability, process consistency, testing, production capacity, and the ability to maintain the approved specifications during volume manufacturing.
Q14: How can I reduce flexible PCB prototype costs?
A14: Prototype costs can be reduced by confirming the design requirements early, avoiding unnecessary complexity, selecting readily available materials, reviewing the stackup, optimizing panelization, and completing DFM before fabrication. However, cost reductions should not compromise the mechanical or electrical requirements of the final application.