HDI PCB 1oz vs 2oz Copper: Where Each Thickness Performs Best in Production
In HDI manufacturing, choosing between 1oz and 2oz copper is not simply a matter of selecting a thicker conductor for higher current. Copper thickness affects routing density, etching behavior, plating requirements, impedance control, thermal performance, panel utilization, and the overall manufacturing process window.
For most density-driven HDI designs, 1oz copper provides a practical balance between fine-line routing and production stability. 2oz copper becomes more attractive when power distribution, current capacity, thermal spreading, or mechanical robustness is more important than maximum routing density. The right choice therefore depends on the electrical requirements and the physical constraints of the complete HDI stackup.
It is also important to distinguish nominal copper weight from finished copper thickness. As a general reference, 1oz copper corresponds to approximately 34.8 µm (1.37 mil), while 2oz corresponds to approximately 70 µm (2.76 mil). Actual finished outer-layer copper can differ because electroplating adds copper during fabrication.

Quick Engineering Comparison: 1oz vs 2oz in HDI Production
The primary difference between 1oz and 2oz copper is the amount of conductive material available on the layer. Doubling copper thickness increases conductor cross-sectional area at the same trace width, which can reduce resistance and improve thermal capacity. However, the additional copper also takes longer to etch and requires more process control to maintain narrow trace geometries.
For HDI boards, this creates a direct trade-off. A thinner copper structure generally gives the fabricator more freedom to maintain fine line/space features, while thicker copper is more suitable when the design requires greater conductor cross-sectional area.
| Factor | 1oz Copper | 2oz Copper |
|---|---|---|
| Typical Min Line/Space (HDI) | 3-4 mil / 3-4 mil | 5-6 mil / 5-6 mil (often 6/6+ safe) |
| Etching Control | Excellent, lower undercut | More lateral etch, trapezoidal traces |
| Plating Time & Uniformity | Faster, standard process | Longer cycles, higher risk of voids in microvias |
| Current Capacity (10mil trace, ~10°C rise) | ~1-1.5A | ~2-2.5A |
| Thermal Performance | Adequate for signals | Better heat spreading |
| Manufacturing Cost | Baseline | +20-40% |
| Production Yield | Higher in fine-pitch HDI | Lower due to etching/plating challenges |
| Lead Time Impact | Standard | Slightly longer |
These differences should be evaluated at the design stage rather than after the stackup has been finalized. IPC design guidance treats conductor size and current-carrying capacity as design parameters, while HDI-specific design requirements are covered by IPC-2226.
Choosing Between 1oz and 2oz Copper for Different HDI PCB Requirements
There is no universal rule that makes 1oz or 2oz the better copper weight for every HDI PCB. The correct selection depends on routing density, current requirements, thermal constraints, layer function, and the manufacturer's process capability.
| If your priority is... | Better Choice | Why |
|---|---|---|
| Finest line/space & HDI density | 1oz | Superior etch control allows reliable 3-4 mil features critical for microvia fanout |
| Highest current per trace or thermal headroom | 2oz | Roughly double cross-section reduces resistance and improves dissipation |
| Lowest cost & fastest turnaround | 1oz | Standard material and processes, better panel utilization |
| Best overall yield in volume production | 1oz | Fewer DFM flags and tighter process window |
| High-reliability power sections in mixed HDI | 2oz (on dedicated layers) | Stronger mechanical traces, better under thermal cycling |
| Extreme fine-pitch BGA escape routing | 1oz | 2oz often forces design compromises or extra layers |
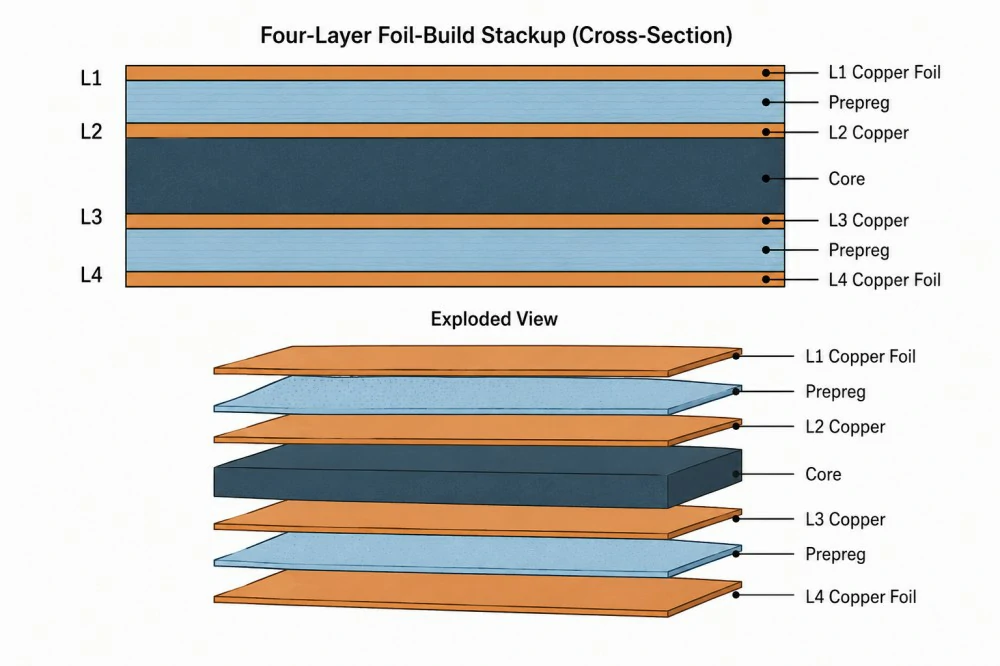
A hybrid stackup is often practical when a board contains both dense signal routing and power sections. For example, an HDI PCB may use 1oz copper on outer routing layers while assigning 2oz copper to selected power or ground layers. This avoids forcing every layer to use the heavier copper specification.
The decision should ultimately be made together with the PCB fabricator because the available line/space window depends on the actual copper system, imaging process, etching process, plating method, and required production yield.
Line Width and Spacing Trade-offs in HDI 1oz vs 2oz Copper
Line width and spacing are usually the first manufacturing considerations when comparing 1oz vs 2oz copper. Thicker copper requires the etching process to remove more material, which increases the challenge of maintaining narrow and accurately defined conductors.
Published manufacturing capabilities illustrate this relationship. For example, one current PCB fabrication capability lists minimum trace/space around 0.09–0.10 mm for 1oz copper and approximately 0.16 mm for 2oz copper, although these are manufacturer-specific values rather than universal HDI limits.
For HDI routing, this difference can become important around fine-pitch BGA packages and microvia fanout regions. When the available routing channel becomes narrower, increasing copper thickness may force wider traces, larger spacing, or additional routing layers.
During CAM review, the fabricator therefore evaluates the relationship between:
- copper weight and finished copper thickness;
- minimum trace width;
- minimum spacing;
- etch compensation;
- copper distribution;
- via and pad geometry;
- impedance requirements; and
- required production yield.
For a density-driven HDI design, 1oz copper often provides more flexibility. This does not mean that 2oz copper cannot be used for HDI; rather, the stackup and routing rules must be designed around the thicker conductor from the beginning.

Copper Weight, Impedance, and Signal Integrity in HDI PCB Designs
Copper thickness also influences signal integrity, but not simply because thicker copper is always electrically better.
For controlled-impedance HDI routing, conductor width, copper thickness, dielectric thickness, dielectric constant, reference-plane position, and copper surface characteristics all interact. Changing from 1oz to 2oz can therefore require an impedance review rather than a simple material substitution.
If a trace becomes thicker while its width and dielectric geometry remain unchanged, its electrical behavior changes. The final impedance target should therefore be recalculated using the actual stackup and finished copper dimensions.
This is particularly important when a design combines high-speed signal layers with 2oz power layers. The copper weight can be different between functional layers, but the stackup still needs to maintain the required electrical relationships.
For high-speed HDI designs, copper roughness and surface characteristics can also influence signal loss at higher frequencies. Copper surface roughness is an established signal-integrity consideration in multi-GHz PCB applications, so material and copper selection should be reviewed together with the frequency range and transmission-line structure.
Copper Thickness and Thermal Performance in Power-Dense HDI Boards
2oz copper becomes more attractive when the board contains localized power-density or thermal-management requirements.
A thicker conductor can reduce DC resistance for a given trace width and provide more copper cross-section for heat spreading. However, the thermal performance of 1oz vs. 2oz copper PCBs depends on the complete thermal path. A 2oz trace connected to a poorly designed thermal structure will not automatically solve a board-level thermal problem.
For power sections, engineers should evaluate:
- trace width and copper cross-section;
- power-plane area;
- via arrays and thermal vias;
- component pad geometry;
- copper distribution;
- board thickness;
- heat transfer into adjacent layers; and
- allowable temperature rise.
In a mixed HDI board, this often leads to a layer-specific solution rather than using 2oz everywhere.
Etching Capability and Yield Impact in HDI Production
Etching is where 2oz copper shows its limitations fastest. Thicker foil means more material to remove, leading to greater lateral etch and trapezoidal cross-sections. This reduces effective conductor width at the base and complicates impedance control. Yield tends to decrease when pushing below 5-6 mil on 2oz because of necking or residual copper issues. 1oz maintains better aspect ratios and process stability, supporting the aggressive features HDI customers expect.
In our experience, attempting tight geometries on 2oz often triggers DFM revisions that add layers or widen the board — driving up final cost despite the "heavier copper" intent.
Reliability Differences Under Real Operating Conditions
2oz copper traces offer better mechanical strength and lower resistance, which helps in high-current or high-vibration environments. However, in pure HDI signal routing the added thickness can introduce more stress at via transitions due to plating challenges. 1oz generally provides balanced reliability with fewer process-induced defects. Long-term, both perform well when designed within limits, but 1oz edges out in high-density boards where via reliability dominates failure modes.
Factory Perspective: How Manufacturers Evaluate HDI 1oz vs 2oz Copper
In DFM review we look first at min feature size against copper weight. 1oz passes most HDI files cleanly with standard etch compensation. 2oz frequently requires adjustments to trace widths, annular rings, and via parameters, plus extra attention to copper balance for warpage control. CAM preparation takes longer for 2oz because of modified tool paths and plating recipes.
Production yield stays higher with 1oz due to process stability and better panel utilization — thicker copper reduces the number of boards per panel slightly and increases scrap risk. Tooling is standard for both but inspection (AOI, cross-section) intensifies on 2oz. We normally recommend 1oz for the majority of HDI builds unless power sections explicitly need the extra capacity. For mixed designs, we suggest 2oz only on internal power planes while keeping outer HDI layers at 1oz.

When 1oz Copper Is the Better Choice for HDI PCB Design
1oz copper is generally more suitable when routing density and fine-feature control are the main priorities of an HDI PCB design. Its lower copper thickness gives the fabrication process more flexibility when forming narrow traces and spaces, which is particularly important around fine-pitch BGA packages and dense microvia fanout regions. For compact boards where every routing channel matters, maintaining a thinner copper structure can help preserve the available routing space without unnecessarily increasing the layer count.
The advantage of 1oz copper is not limited to line width and spacing. A thinner copper structure also simplifies etching and artwork compensation, giving the fabricator a more manageable process window for fine-line features. This can be especially valuable in volume production, where small variations in etching, copper distribution, and panel processing can accumulate across large production panels.
For signal-dominated HDI boards, 1oz copper is often a practical starting point when the required current can be achieved through appropriate trace width, copper distribution, and thermal design. High-speed signal layers, BGA escape regions, and microvia-heavy routing areas generally benefit more from routing flexibility than from the additional copper cross-section provided by 2oz material. The final decision should still be confirmed against the manufacturer's actual line/space and finished-copper capability rather than a generic 1oz design rule.
When 2oz Copper Is the Better Choice for HDI PCB Design
2oz copper becomes more relevant when electrical or thermal requirements place greater emphasis on conductor cross-section than on maximum routing density. At the same trace width, the thicker copper provides a larger conductive cross-section, which can reduce resistance and support higher current capacity when the thermal conditions and allowable temperature rise are properly considered.
This makes 2oz copper useful for power distribution, ground structures, and other sections where current flow or heat spreading is a significant design concern. In a high-power HDI board, for example, selected 2oz layers can provide additional copper where power density is concentrated without requiring every signal layer to use the same thickness.
The trade-off is that thicker copper places greater demands on etching and dimensional control. If a 2oz layer also needs to accommodate fine-pitch routing, the heavier copper may require wider traces or spacing and can reduce the routing flexibility available to the designer. For this reason, 2oz copper is usually most effective when the board has sufficient routing space or when the electrical benefit clearly justifies the additional manufacturing constraints.
A layer-specific approach can therefore be more practical than specifying 2oz copper throughout the entire HDI PCB. Using 2oz on selected power or ground layers while retaining 1oz on dense signal layers can provide the additional current and thermal capacity where it is needed without imposing the same routing limitations across the whole stackup.
Practical Decision Guide: 1oz vs 2oz Copper for HDI PCBs
The decision between 1oz and 2oz copper should begin with the function of each layer rather than with copper weight alone. If the primary challenge is fitting fine-pitch routing, microvia fanout, and controlled-impedance signals into a compact HDI stackup, 1oz copper will generally provide more manufacturing flexibility. If the board instead contains power-intensive sections where conductor resistance, current capacity, or thermal spreading becomes a dominant concern, 2oz copper may offer a more appropriate electrical structure.
The routing requirements should then be checked against the fabricator's actual process capability. A copper weight that works well on a relatively open power layer may create unnecessary constraints on a dense BGA escape layer. The same board can therefore legitimately use different copper weights on different layers. This is particularly useful for complex HDI designs that combine high-density signal routing with localized power requirements.
From a manufacturing perspective, the most practical solution is the one that balances electrical performance with the available process window. Copper thickness affects etching, trace geometry, plating, impedance, panel utilization, and potentially the number of layers required to complete the routing. A seemingly simple decision to increase copper from 1oz to 2oz can therefore influence the entire stackup and manufacturing cost if the original routing geometry was designed around thinner copper.
For this reason, copper selection should be reviewed during stackup development and CAM/DFM preparation rather than after the layout is finished. When 1oz copper satisfies the electrical and thermal requirements, it can preserve routing density and simplify fine-line fabrication. When 2oz is required for specific power or thermal functions, limiting the heavier copper to those layers can avoid unnecessary compromises elsewhere in the HDI structure.
In practice, the best 1oz vs 2oz copper strategy is often a balanced one: use the thinner copper where routing density and fine-feature control matter most, and introduce thicker copper only where the electrical or thermal requirements justify it. This layer-specific approach gives the PCB designer and manufacturer greater freedom to optimize the HDI stackup for both production reliability and board performance.
FAQ
Q1: What Is the Main Difference Between 1oz and 2oz Copper in an HDI PCB?
A1: 1oz copper has a nominal thickness of about 34.8 µm, while 2oz copper is about 70 µm. The thicker copper provides greater conductor cross-sectional area and can support higher current or thermal requirements at the same trace width. However, it also makes fine-line etching more difficult. The practical choice depends on routing density, electrical requirements, stackup, and the PCB manufacturer's process capability.
Q2: Is 1oz or 2oz Copper Better for Fine-Pitch HDI Routing?
A2: 1oz copper is generally more suitable when fine-pitch HDI routing is the primary requirement. Thinner copper typically provides a wider manufacturing window for narrow traces and spaces because less copper must be removed during etching. However, the exact minimum line/space depends on the fabricator's imaging and etching process. Designers should confirm the actual production capability before committing to a specific geometry.
Q3: How Does 1oz vs 2oz Copper Affect PCB Cost?
A3: 2oz copper can increase manufacturing cost, but there is no universal percentage that applies to every HDI PCB. The final impact depends on copper material, plating, etching, panel utilization, board geometry, layer count, production volume, and whether heavier copper forces routing or stackup changes. A cost comparison should therefore evaluate the complete fabrication specification rather than applying a fixed 20–40% surcharge.
Q4: How Does Copper Thickness Affect HDI PCB Current Capacity?
A4: Increasing copper thickness increases conductor cross-sectional area, which can improve current-carrying capability at a given trace width. However, current capacity is also affected by trace width, temperature-rise limits, board thickness, material, copper planes, and whether the conductor is internal or external. IPC-2152 provides guidance for evaluating these variables, so fixed amp ratings should not be applied universally to 1oz or 2oz copper.
Q5: What Is a Typical 1oz Copper Thickness?
A5: 1oz copper corresponds to approximately 34.8 µm, or about 1.37 mil, as a nominal foil thickness. The actual finished copper thickness can differ, particularly on outer layers where electroplating adds copper during fabrication. For production specifications, engineers should clarify whether the stated 1oz requirement refers to starting foil, finished copper, or another controlled thickness requirement.
Q6: When Should I Use 2oz Copper PCB Layers in an HDI Design?
A6: 2oz copper PCB layers are useful when power distribution, current capacity, thermal spreading, or mechanical robustness is more important than maximum routing density. Typical applications include power rails, ground structures, and selected power sections of mixed HDI boards. If dense BGA escape routing is also required on the same layer, the designer should confirm that the fabricator can achieve the required line/space with 2oz copper.
Q7: Can an HDI PCB Use Both 1oz and 2oz Copper?
A7: Yes. A hybrid copper structure can assign different copper weights to different layers according to their electrical and routing functions. For example, 1oz copper can be used on dense HDI signal layers while 2oz copper is assigned to selected power or ground layers. This approach can preserve routing density while providing additional conductor cross-section where current or thermal requirements justify it.