




In surface-mount manufacturing, soldering is an art, but reliability is a science. For high-density, high-reliability products such as servers, base stations, and high-end switches, passing functional electrical test (FCT) is far from sufficient. If a board suffers from plated-through hole copper fracture, conductive anodic filament (CAF) leakage, or gold-finger oxidation leading to contact failure after a few months in the field, the result can be a costly recall. This article details essential PCB reliability test items, their test methods, and engineering acceptance criteria.
Whether you are a layout engineer, a process engineer, or a quality manager, the following serves as a practical, engineering-focused guide.
Chapter 1: Gold Fingers — Nitric Acid Vapor Corrosion Resistance Test
Gold fingers are the critical contact interface between a board and its mating connector. Although the gold finish (typically ENIG or electrolytic hard gold) provides excellent conductivity and oxidation resistance, porosity in the plating can allow nitric acid vapor to penetrate to the underlying nickel/copper. In humid environments that accelerates electrochemical reactions, elevates contact resistance, and degrades long-term contact reliability.
1.1 Why use nitric acid vapor-
Nitric acid vapor testing follows established standards (EIA 364-53B, ASTM B735-95, IPC-TM-650, ISO 14647:2000). Nitric acid vapor is highly sensitive to micro-pores in the gold layer; it readily reaches and reacts with the underlying metal, producing visible blue/green corrosion spots that reveal the density and integrity of the plating.
1.2 Step-by-step procedure
Phase 1: Rigorous pre-clean
-
Cleaning: Ultrasonically clean with methanol, isopropyl alcohol, or acetone for 30 seconds to remove organics such as fingerprints, oils, and flux residues.
-
Drying: Blow dry with filtered compressed air at a pressure below 30 psi. Excessive pressure can damage the plated structure.
-
Microscopic inspection: Verify cleanliness at 10× magnification. This step is often overlooked. Dust particles can retain nitric acid and cause false failures.
Phase 2: Nitric acid vapor exposure (chemical development)
-
Chamber preparation: Use a large desiccator (approximately 9–12 L). Pour 500 ml of concentrated nitric acid with appropriate safety controls.
-
Sample placement:
-
The test area must be > 75 mm above the liquid surface. Too close risks droplet splatter; too far reduces vapor concentration.
-
Maintain > 25 mm from the chamber wall.
-
Maintain sample-to-sample spacing > 12 mm to prevent cross-contamination.
-
-
Environmental control: Seal for 60 ± 5 minutes. Maintain ambient at 24 ± 3 °C and relative humidity < 60%. Elevated humidity dilutes the nitric acid vapor and invalidates the test.
Phase 3: Post-treatment and evaluation
-
Neutralization: Immerse in 5% NaOH for 25–30 seconds to terminate the reaction.
-
Rinse and dry: Rinse with tap water for 5 seconds, then dry in an oven at 125 °C for 10–15 minutes.
-
Microscopy: After cooling to room temperature, inspect at 20–50× magnification.
1.3 Pass/fail criteria
Do not fail samples merely for the presence of dark spots. Define and assess the evaluation window as follows:
-
Exclude edge effects: Do not consider spots within 0.5 mm from the front and rear edges of the gold finger, and 0.15 mm from its left and right edges.
-
Core evaluation region: Within the central area, locate the most severely corroded region and assess a circular window with 1 mm diameter. If the gold-finger width is less than 1 mm, use its actual width as the evaluation width.
Acceptance criteria (all must be met):
-
Count of spots sized 0.05–0.12 mm: ≤ 8 within the 1 mm window.
-
Count of spots sized 0.12–0.4 mm: ≤ 2 within the 1 mm window.
-
Zero tolerance: No spot > 0.4 mm is permitted.
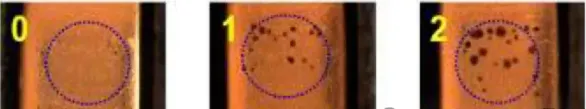
Engineering note: If corrosion spots merge into patches or exhibit a "map-like" spread, the sample should be rejected even if counts appear within limits. This often indicates insufficient gold coverage over electroless nickel or abnormal phosphorus content in ENIG, leading to porosity or black-pad tendencies.
Chapter 2: Thermal Stress Testing
SMT soldering induces severe thermal shocks. With lead-free processes peaking at up to 260 °C, both laminate and plated-through hole (PTH) copper must withstand significant thermal stress. Two methods are commonly used: solder float and reflow profiling. When results conflict, reflow testing is the final arbiter because it replicates production thermal exposure more realistically.
2.1 Parameters: solder float vs. reflow
| Test item | Process type | Temperature | Time/condition | Repetitions | Arbitration role |
|---|---|---|---|---|---|
| Solder float | Lead-free | 288 ± 15 °C | 10–11 s | 3 | Reference |
| Reflow | Lead-free | Peak 260 ± 5 °C | ≥ 217 °C for 120–150 s; ≥ 255 °C for 20–30 s | 5 | Final arbitration |
Interpretation:
-
Solder float approximates the instantaneous high temperature of wave or manual soldering. The bath at 288 °C challenges the laminate's glass transition temperature (Tg) and resin robustness.
-
Reflow emulates SMT production. Five reflow cycles subject the board to repeated room-temperature to 260 °C excursions, stressing Z-axis CTE mismatch between resin, glass fabric, and copper plating.
2.2 Cross-section evaluation
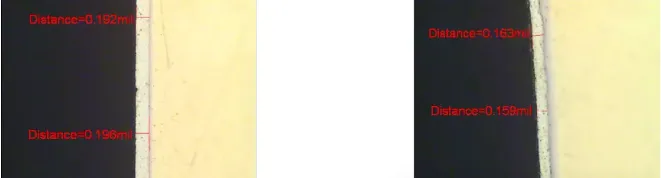
External appearance must show no blistering and no solder mask lifting. Final judgment requires metallographic cross-sectioning (microsection/cross section).
Reject if any of the following are observed:
-
No cracks allowed in laminate or plated copper. Corner cracks at hole entry/exit are common signs of Z-axis expansion straining the hole wall copper.
-
No delamination within the laminate or between prepreg layers. Typical causes include high moisture uptake, insufficient resin cure, or weak resin-to-glass bonding.
Chapter 3: CAF Resistance Testing
Conductive anodic filament (CAF) is a latent failure mode in dense PCBs. Under an applied potential and moisture/heat, anodic copper can dissolve and migrate along glass-resin interfaces, ultimately forming metallic dendrites at the cathode and causing short circuits. The test design accelerates this mechanism to screen materials and processes.
3.1 Test logic and steps
-
Preconditioning: Subject samples to five lead-free reflow cycles to activate internal stresses and emulate real production exposure.
-
Phase 1 (static screening): 85 °C/85% RH, no bias, for 96 hours. Measure insulation resistance R1.
-
Logic: If R1 ≤ 10 MΩ without bias, the material is too hygroscopic or has intrinsically poor insulation. Reject.
-
-
Phase 2 (biased acceleration): 85 °C/85% RH with 50 VDC applied for 240 hours. Monitor insulation resistance R2 continuously.
-
Failure criteria: Final R2 < 100 MΩ, or three or more recorded events of R2 < 100 MΩ during the test, constitutes failure.
-
Note: A 50 VDC bias is an appropriate acceleration factor for server-class boards where adjacent planes may differ by 12–48 V. A 240-hour duration accelerates field-aging behavior to a practical timeframe.
Chapter 4: Electrical and Insulation Tests
To ensure electrical safety under harsh environments, three core tests are applied: dielectric withstanding voltage (DWV), insulation resistance (IR), and environmental exposure combined with retest after conditioning.
4.1 Dielectric Withstanding Voltage (DWV)
DWV is a high-stress test of insulation strength.
-
Preconditioning: Five lead-free reflow cycles to reveal micro-cracking, if present.
-
Test coupons: Use Y-pattern or comb electrodes. Comb structures introduce strong field non-uniformity, improving sensitivity to weak points.
-
Condition: Ramp at 100 V/s to 500 +15/-0 V and hold for 30 s.
-
Acceptance: Leakage current ≤ 0.5 mA. Any arc-over or dielectric breakdown, even momentary, is a failure.
4.2 Insulation Resistance (IR)
This test evaluates long-term insulation stability under humid heat.
| Condition | IR requirement | Appearance |
|---|---|---|
| Initial (room temperature) | ≥ 500 MΩ | - |
| After humid heat | ≥ 100 MΩ | No blistering, delamination, or other anomalies 24 hours after test end |
Important: After humid heat IR testing, repeat the DWV test. Some materials show reduced dielectric strength when moisture-laden. If DWV still passes after drying, recovery is acceptable; persistent leakage after drying indicates irreversible damage.
Chapter 5: Environmental Robustness — Thermal Shock and IST
5.1 Thermal shock (-55 °C to +125 °C)
Thermal shock simulates harsh transport or operating conditions, e.g., moving between sub-zero and high-temperature environments.
-
Condition: -55 °C to +125 °C, 200 cycles.
-
Monitoring: Daisy-chain interconnect resistance measured after the first and after the final cycle.
-
Acceptance: Resistance change ΔR < 10%. Sudden increases indicate micro-cracks or fractures in interconnects or plating.
5.2 Interconnect Stress Test (IST)
IST is a high-acceleration reliability test that heats interconnects electrically rather than by air exchange.
-
Principle: Apply current to internal plated through-hole chains: "P" (via chains) and "S" (pad chains). Joule heating raises coupon temperature from ambient to 150 °C in approximately 3 minutes.
-
Target: All boards must endure ≥ 250 cycles.
-
Failure criterion: ΔR > 10% on the monitored chain indicates failure.
-
Advantages: IST is more than ten times faster than conventional thermal shock and directly stresses PTH walls, exposing weak points in hole plating more effectively.
Chapter 6: Process Controls — Prevent Failures at the Source
With the tests and criteria in mind, designers and SMT/process engineers can deploy targeted controls to reduce risk.
6.1 Gold-finger porosity mitigation
-
Design: Specify nickel thickness at 3–5 μm and gold thickness at 0.05–0.1 μm for ENIG or appropriate hard-gold processes. Gold too thin fails to cover nickel porosity; gold excessively thick can embrittle soldered joints.
-
Process: Maintain ENIG bath activity tightly and replace baths regularly to avoid black-pad conditions.
6.2 Thermal stress and CAF risk reduction
-
Laminate selection: For server boards, use high-Tg (≥ 170 °C) materials with moderate/low CTEs (e.g., IT180A, EM-827 or equivalent high-reliability grades).
-
Drilling: Hole wall roughness is a CAF pathway. Use fresh drill bits or laser drilling where appropriate to minimize glass fiber pull-out and reduce moisture/electrolyte pathways along the glass-resin interface.
-
Desmear: Apply robust desmear/etchback so resin is properly recessed and glass fibers are exposed for better copper adhesion, reducing delamination and improving thermal shock tolerance.
6.3 IST and thermal shock robustness
-
Hole copper thickness: For lead-free assemblies, specify minimum 25 μm (1 mil) PTH copper. For high-reliability boards, 30 μm or more is recommended to increase fatigue life.
-
Aspect ratio: Keep PTH aspect ratio ≤ 8:1 where possible. Excessive aspect ratio impedes solution exchange during plating, thinning copper at hole centers and elevating IST failure risk.
Chapter 7: One-Glance Summary of Seven Key Tests
The table below consolidates the core stresses, acceptance criteria, and engineering role for each test.
| # | Test | Primary stress | Key criteria | Engineering role |
|---|---|---|---|---|
| 1 | Nitric acid vapor on gold fingers | Chemical corrosion (porosity → nickel attack) | Within 1 mm window: small spots ≤ 8, medium spots ≤ 2, none > 0.4 mm | Gatekeeper for contact reliability |
| 2 | Thermal stress (solder float + reflow) | Extreme thermal shock → Z-axis CTE mismatch | No blisters; cross-sections free of cracks/delamination | Baseline for laminate and PTH thermal robustness |
| 3 | CAF resistance | Hot/humid bias → electrochemical migration | R1 > 10 MΩ; R2 ≥ 100 MΩ throughout | Defense against long-term insulation degradation |
| 4 | DWV | High electric field → arc-over/breakdown | 500 V/30 s; I_leak ≤ 0.5 mA; no arc-over or breakdown | Insulation safety margin |
| 5 | IR | Extended humidity/heat → moisture uptake, leakage | Initial ≥ 500 MΩ; post-humidity ≥ 100 MΩ; no blisters/delamination; passes repeat DWV | Insulation health under humid heat |
| 6 | Thermal shock (TC) | Repeated expansion/contraction → PTH/interface fatigue | ΔR < 10%; cross-section OK; 200 cycles, -55 °C to +125 °C | Thermo-mechanical fatigue screen |
| 7 | IST | Direct Joule heating → accelerated PTH fatigue | ≥ 250 cycles; ΔR ≤ 10% | Accelerated verification of hole copper life |
Conclusion
Design is the source, laminate is the foundation, process is the guarantee, and testing is the bottom line. By understanding the physical and chemical mechanisms behind each reliability test, engineering teams can move beyond basic manufacturing to robust, repeatable, and predictable product performance in the field.