In surface-mount technology (SMT), forming reliable solder joints depends on two closely linked concepts: wetting at the interface between molten solder and the base metal, and the inherent solderability of the materials being joined. Wetting describes how solder spreads across a surface and interacts at the atomic level, while solderability describes the ability of a component lead or PCB pad to achieve wetting under specified process conditions. Together, they determine whether a joint will achieve strong metallurgical bonding, stable electrical contact, and long-term reliability.
Surface Wetting
Wetting is the phenomenon where molten solder spreads and covers the surface of the metal being soldered. When wetting occurs, atoms from the liquid solder and the base metal interdiffuse at the interface and form intermetallic compounds (IMCs). This solid-state reaction is characteristic of successful soft soldering and is essential for both mechanical adhesion and low-resistance electrical contact.
Simply immersing a solid metal coupon into a bath of molten solder creates physical contact, but that does not guarantee wetting. A surface barrier—most commonly an oxide film or organic contamination—can prevent the intimate contact needed for atomic diffusion. Only after removing the part from the solder can we evaluate whether wetting has occurred by observing spreading and surface coverage.
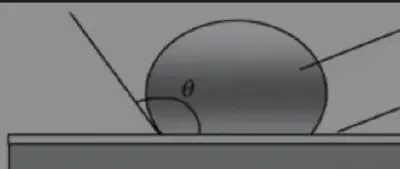
Wetting occurs only when the molten solder is in intimate, clean contact with the base metal surface, creating sufficient interfacial attraction. If a tenacious contaminant—such as an oxide layer, moisture, flux residue, or oil—remains on the surface, it acts as a barrier to solder bonding and obstructs wetting. On a contaminated surface, a droplet of solder behaves much like a droplet of water on an oily plate: it beads up, fails to spread, and exhibits a large contact angle.
On a contaminated surface, solder does not spread and the contact angle θ is greater than 90°, indicating non-wetting behavior.
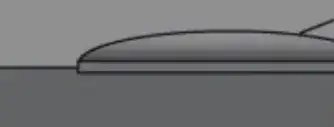
If the solderable surface is clean, the metal atoms at the interface are brought sufficiently close for interdiffusion and bonding. Wetting proceeds, solder spreads across the contact surface, and a thin IMC layer forms at the interface, providing mechanical anchoring and good electrical contact.
Contact Angle and Surface Energy
The degree of wetting is commonly described by the contact angle θ at the triple line where solder, solid, and atmosphere meet. Qualitatively, small θ indicates good wetting, extensive spreading, and strong interfacial bonding; large θ indicates poor wetting and weak interfacial attraction. Contact angle is governed by the balance of surface energies: solder surface tension, solid surface energy, and the interfacial energy between solder and solid. Flux chemistry, the cleanliness of the base metal, the solder alloy, the reflow atmosphere, and temperature all influence this energy balance and therefore the observed wetting.
Role of Flux and Atmosphere
Flux is critical to wetting. It dissolves or reduces surface oxides, protects the interface from further oxidation during heating, and can lower the effective interfacial energy, all of which promote solder spreading. However, flux has an activation temperature window. If the assembly is overheated or held at elevated temperature too long, flux activity degrades and oxides can reform before a reliable joint is established. The reflow atmosphere also matters: nitrogen environments suppress oxidation during heating, which can improve wetting on sensitive finishes, while air reflow is more prone to re-oxidation of exposed copper or tin surfaces.
Intermetallic Compound Formation
As wetting proceeds, a thin intermetallic compound layer grows at the solder–base metal interface. This layer anchors the joint metallurgically. Very thin, continuous IMC is beneficial for bond strength; excessively thick or brittle IMC can degrade mechanical reliability. IMC growth is driven by time and temperature during soldering and will continue slowly during service. A properly controlled thermal profile establishes sufficient IMC for adhesion without promoting excessive growth.
Thermal Profile and Heat Capacity Effects
Wetting is time–temperature dependent. The materials' heat capacities (thermal mass) influence how quickly the joint area reaches solder liquidus and how long it remains above liquidus. Components with high thermal mass (large ground pads, heat slugs, or heavy copper planes) can lag in temperature, delaying flux activation at the interface and shortening effective wetting time. Conversely, overheating small components can burn off flux prematurely and drive dewetting. A balanced reflow profile—preheat, soak (if used), and time above liquidus—must be tuned to the assembly's thermal distribution to support consistent wetting across all joints.
Solderability
Solderability is the capability of the base materials to be soldered under specified time and temperature conditions. It depends on the thermal characteristics of the parts being soldered (components and pads), the applied heating profile, and, crucially, the cleanliness and chemical state of the solderable surfaces. Good solderability means that, within the available process window, the surface can be wetted promptly to form a continuous solder layer and a sound IMC interface.
Solderability correlates strongly with wetting because both are ultimately about forming a clean, active interface. A surface with poor solderability will resist wetting even if the process conditions are nominal. Common contributors to reduced solderability include oxidation from improper storage, aging of protective finishes, contamination from handling, reaction products from solder mask or board fabrication residues in the pad area, and damaged or porous plating on component leads.
How Solderability Is Evaluated
Two common evaluation methods are used in manufacturing and incoming inspection:
- Dip (immersion) testing: A sample lead or pad coupon is immersed in molten solder under controlled conditions. After withdrawal, the surface appearance indicates wetting quality. The test assesses whether the surface wets within the specified time and temperature window.
- Wetting balance testing: This method measures the wetting force exerted on a sample versus time during immersion in molten solder. It quantifies key parameters such as time-to-wet and maximum wetting force, providing a more sensitive assessment than visual inspection alone.
Both methods are fundamentally evaluating the same behavior: whether the surface can be wetted within a controlled process window and how robust that wetting is.
Observations in Dip Testing
When a sample is withdrawn from a solder bath, one or more of the following conditions may be observed:
- Non-wetting: The surface emerges essentially uncovered by solder, with no visible interaction. The substrate retains its original color or finish. This typically occurs when the surface oxide is too thick or tenacious for the flux to remove within the effective soldering time.
- Wetting: After draining away the molten solder, a thin solder layer remains on the surface, indicating interfacial interaction and IMC formation. Complete wetting leaves a smooth, uniform, crack-free solder film that adheres well to the substrate.
- Partial wetting: Some areas exhibit wetting while others remain unwetted. This often points to localized contamination, uneven heating, or variable surface condition across the pad or lead.
- Dewetting: The surface initially wets, but the solder subsequently recedes into droplets, leaving only a very thin film in the previously wetted areas. Dewetting can be driven by contamination, oxidation during prolonged or excessive heating, incompatible flux/surface chemistry, or degraded finishes.
Typical Causes and Corrective Actions
Understanding the root causes of weak or inconsistent wetting helps drive effective process and materials controls:
- Surface oxides and contamination: Oxidation of copper, tin, or nickel surfaces, as well as oils from handling or residues from fabrication, impede wetting. Corrective actions include improved storage and packaging, minimizing exposure before assembly, controlled handling with gloves, pre-cleaning where appropriate, and selecting fluxes with suitable activity for the surface condition.
- Finish condition and aging: Solderable finishes (e.g., organic protective films or plated coatings) can degrade over time via oxidation or diffusion, reducing solderability. Manage shelf life, monitor incoming quality, and use appropriate storage conditions (dry, sealed, and temperature-controlled). For borderline finishes, nitrogen reflow can mitigate oxidation during heating.
- Thermal imbalance: Pads tied to large copper planes or thermal slugs can remain cooler than surrounding joints, delaying flux activation and shortening effective time above liquidus. Tune the reflow profile or use thermal relief patterns in the PCB design to balance heat flow. Verify uniform wetting across components with both light and heavy thermal masses.
- Flux selection and process window: Flux with insufficient activity for the surface condition or applied outside its activation window can result in partial wetting or dewetting. Match flux chemistry to the finish and oxidation risk, and set preheat, soak, and peak temperatures to maintain flux activity through the wetting interval.
- Atmosphere: Air reflow increases the risk of re-oxidation during heating, especially for bare copper or thin tin finishes. Nitrogen reflow reduces oxidation and can significantly improve wetting margins on sensitive surfaces.
- Solder paste deposition: Extremely low paste volume can hinder spreading and coverage, while excessive paste can mask underlying solderability issues until late in reflow. Verify stencil design and transfer efficiency to ensure consistent deposit heights and volumes.
Practical Guidance for Robust Wetting and Solderability
- Maintain surface cleanliness: Keep the PCB panel and component sealed until use. Avoid fingerprints and airborne contaminants. If cleaning is used, ensure the process is compatible with the finishes and does not leave harmful residues on pads.
- Control storage and shelf life: Adhere to supplier-recommended storage conditions for boards and components. Track lot dates and shelf life for sensitive finishes, and rotate inventory to minimize aging.
- Tune the reflow profile: Validate preheat rate, soak duration (if applicable), peak temperature, and time above liquidus to align with the thermal mass distribution of the assembly. Confirm that flux remains active until wetting completes, and avoid excessive thermal exposure that can cause dewetting.
- Select appropriate flux and alloy: Choose solder paste with the right flux activity for the finish and cleanliness level expected in production. Verify alloy and flux compatibility with component lead platings and PCB finishes through process trials.
- Consider atmosphere control: For products with marginal solderability or tight reliability requirements, nitrogen reflow is often justified to expand process margin.
- Inspect and monitor: Use cross-sections, wetting balance data, and joint appearance criteria to monitor wetting quality. Pay attention to changes in joint luster, coverage uniformity, and occurrence of dewetting or non-wetting defects, and feed findings back into materials and process controls.
Ultimately, wetting and solderability are two sides of the same metallurgical coin. Wetting describes the interfacial behavior of molten solder on a specific surface under given conditions; solderability describes how readily that behavior is achieved across the range of conditions available in manufacturing. By ensuring clean and stable surfaces, selecting appropriate materials, and tightly controlling the thermal and chemical environment during reflow, SMT processes can consistently produce joints with continuous solder coverage and robust IMC formation—and thereby deliver reliable electrical and mechanical performance.