During CAM review of an 8-layer HDI order, the specified process edges of 4 mm on all sides prevented a workable 5x3 panel layout. The board thickness of 0.8 mm, TG170 material, immersion gold finish, blind vias, and aluminum plug holes required careful production preparation before the job could move to fabrication. Our CAM engineer adjusted the panelization to 2 mm top/bottom board spacing and 8 mm left/right process rails, producing a finished panel size of 113.5 mm by 118 mm. This change, together with confirmation of production markings and solder mask openings, completed the manufacturing package and allowed production release without downstream delays.
8-Layer Order Parameters and Panelization Requirements
The order ( #HDI-20260410-032 ) called for HDI Shengyi S1000-2M material, eight layers, 0.8 mm finished thickness, 1 oz copper on inner and outer layers, and immersion gold with 2 µ" gold thickness. Blind vias were required (HDI stage 1), vias were to be aluminum plug holes, solder mask was green on both sides, and no silk screen was specified. Separation was mechanical forming with routing, and the panel method was listed as 5x3 with process edges of 4 mm on all four sides. Electrical test was 100% flying probe, and delivery included electrical performance reports and a quality assurance certificate. Acceptable X-out boards were permitted, and production confirmation was marked no.
Panelization is the foundation of efficient PCB manufacturing for this type of order. A 5x3 array multiplies throughput on drilling, plating, imaging, and routing equipment. Process rails (also called process edges or breakaway rails) supply the rigid border needed for automated handling, tooling hole placement, fiducial registration, and depanelization. On a 0.8 mm eight-layer board the rails also limit flex during transport between process steps. The original 4 mm all-around specification produced a panel dimension that could not be nested within standard working area limits while maintaining the required board-to-board clearance for mechanical routing. Without a corrected layout the job could not enter the panelization and tooling-hole programming stage.
Additional preparation items included the factory production number and solder-mask opening definitions. The customer documentation indicated a production number should be added, yet the supplied data contained no character layer. Solder-mask openings were defined as internal openings, and some openings connected across copper traces. Both items required explicit confirmation before the manufacturing files could be frozen.
Panel Size Conflict and Process Rail Adjustment
Our CAM engineer loaded the Gerber and drill data and applied the stated 4 mm process edges on all sides. The resulting panel exceeded the usable working area once the 5x3 array, board-to-board gaps, and equipment clearances were included. Standard process-edge widths of 5–10 mm are common for tooling and AOI registration; 4 mm all around left insufficient margin on the longer axis while over-consuming material on the shorter axis. For a 0.8 mm board, narrower rails also reduce panel stiffness during drilling and plating, increasing the risk of registration shift on the HDI PCB blind-via layers.
Further verification showed that a 2 mm routed gap top and bottom, combined with 8 mm process rails on the left and right, produced a panel of 113.5 mm by 118 mm. The wider left/right rails accommodate standard 3.0–3.2 mm tooling holes and fiducials while giving the mechanical router a stable path. The 2 mm top/bottom spacing matches typical routing-bit clearance and keeps residual web stress low during depanelization. Because the board is only 0.8 mm thick, the adjusted rails also improve flatness during lamination and subsequent imaging of the outer layers. IPC-2221 guidance on feature location and fabrication allowances supports maintaining adequate border material so that drill and routing tolerances do not encroach on active circuitry.
The optimized layout preserves the 5x3 array count, improves material utilization relative to an oversized panel, and keeps the process rails compatible with existing fixture and conveyor systems. If the original 4 mm specification had been forced, the panel would have required a non-standard working size, custom fixtures, or a reduction in array count—all of which lengthen setup time and raise cost per board. With customer confirmation of the 113.5 mm by 118 mm panel and the revised rail widths, the panel drawing and NC routing program could be finalized.

Figure 1: The resulting panel size would be 113.5*118
Production Number and Character-Layer Confirmation
The order parameters included the instruction to add the production factory code. Traceability markings such as serial numbers, date codes, or factory codes are normally placed on the process rail or in a non-functional area so that each panel or lot can be identified through drilling, plating, etching, and final inspection. On this job the supplied fabrication data contained no silk-screen or character layer. Adding a production number would have required inventing a character placement, font size, and location that were not defined by the customer.
Our CAM engineer noted that the absence of a character layer made the marking request unexecutable without additional design input. Because the HDI board already carried no silk screen on either side, any added text would have been the only legend present and could interfere with solder-mask or copper features if placed incorrectly. The practical recommendation was to omit the production number for this lot and rely on the electronic lot tracking already used for the 100% flying-probe test and quality reports. Customer confirmation of this omission removed the open item and allowed the manufacturing package to proceed without a pending character-layer edit.
Omitting an undefined marking avoids the risk of an incorrect or unreadable code that later fails AOI or manual traceability checks. When a production number is required, it is normally laser-marked or ink-printed on the process rail after the panel is complete; the rail width established in the optimized layout (8 mm left/right) provides sufficient area for such marking if it is requested on future revisions.
Solder-Mask Opening Definitions and Trace Exposure
The original solder-mask data defined internal openings, and several openings connected to one another. In a subset of those connections the mask opening crossed copper traces. An opening that bridges a trace leaves the copper exposed after etching and plating. On an immersion-gold board the exposed copper can oxidize, create a solder-wicking path, or reduce the effective insulation between adjacent nets. IPC-A-600 acceptability criteria address solder-mask coverage and exposed copper; incomplete coverage over conductors is normally treated as a defect unless the design explicitly requires it.
Despite the exposure risk, the customer documentation and the EQ response both indicated that the original mask openings should be followed. Our CAM engineer therefore retained the supplied mask geometry rather than modifying the openings or adding mask dams. The confirmation step documented that the connected openings and the resulting trace exposure were accepted as design intent. This decision kept the manufacturing files identical to the approved Gerber set and eliminated the need for a mask-layer edit that could have delayed imaging.
Because the board uses aluminum plug holes and blind vias, the solder-mask process must also accommodate the plugged via topography. Retaining the original openings ensured that any mask clearance already designed around the plug locations remained unchanged. The green mask color and the absence of silk screen further simplified the imaging and developing steps once the opening geometry was locked.

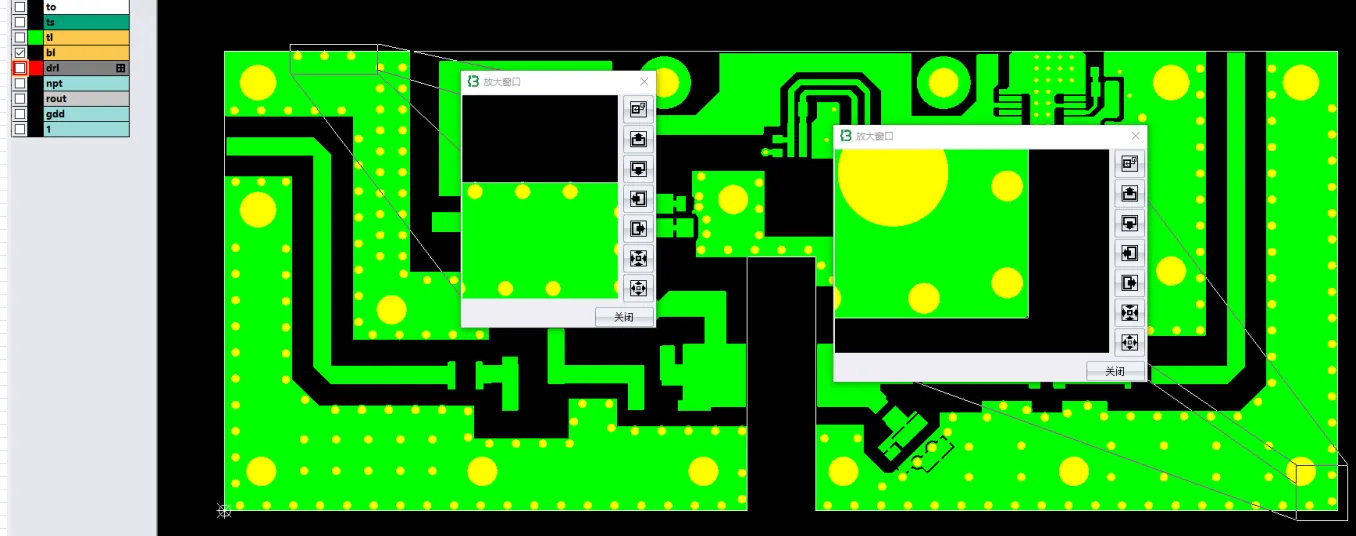
Figure 2: The solder mask opening shown in the file is an internal opening.

Figure 3: The solder mask openings are connected, and some of the connecting openings overlap the traces
Optimization Strategy for Panel Utilization and Process Flow
With the panel size and rail widths confirmed, the manufacturing package could be optimized for the existing process line. The 8 mm left and right rails supply space for a pair of 3.2 mm tooling holes and global fiducials that align the panel in drilling, AOI, and routing. The 2 mm top and bottom gaps allow a standard 1.6–2.0 mm routing bit to separate the boards cleanly without leaving a thick web that would require secondary breaking. On a 0.8 mm eight-layer stack the reduced web also lowers the chance of edge delamination or copper tear-out during mechanical forming.
Material utilization improved because the final 113.5 mm by 118 mm panel fits standard working blanks without excess border waste. The 5x3 array remains intact, so the number of boards per panel—and therefore the amortization of setup, plating, and test time—stays at the planned level. Flying-probe test fixtures can be programmed to the confirmed panel coordinates, and the electronic reports already required by the order can be generated against the same panel identity used for lot tracking.
The same rail geometry supports downstream SMT if the boards are later assembled in panel form. Fiducials on the rails give the pick-and-place machine a stable reference independent of individual board features. Because no silk screen exists, any assembly-side markings would also be placed on the rails; the 8 mm width provides that option without encroaching on the active area. For the bare-board stage the confirmed package already includes the mechanical routing program, the solder-mask artwork matching the original openings, and the decision to omit an undefined production number. These elements together remove the open engineering questions that would otherwise hold the job at the CAM release gate.
Production Readiness Checklist
- Process rails confirmed at 8 mm left/right and 2 mm top/bottom board spacing; panel size 113.5 mm × 118 mm accepted.
- Tooling-hole locations defined on the wider rails for drilling and routing registration.
- Fiducial placement reserved on process rails for AOI and potential panel assembly alignment.
- Production number omitted per confirmation; no character layer added.
- Solder-mask openings retained exactly as supplied, including connecting openings over traces.
- Mechanical routing program generated for the confirmed array and gaps.
- 100% flying-probe test coordinates locked to the final panel layout.
- Manufacturing files (Gerber, drill, mask, panel drawing) released for fabrication.
Each item on the checklist corresponds to an open question that existed after the initial data load. Closing them converted the customer Gerber set into a production-ready package that the shop floor can run without further interpretation.
Final Production Outcome
The engineering preparation produced a manufacturable 5x3 panel of 113.5 mm by 118 mm with process rails sized for tooling, fiducials, and mechanical routing. Customer confirmation of the rail adjustment, the decision to omit the undefined production number, and the instruction to follow the original solder-mask openings removed the remaining holds. The resulting manufacturing package supports the 0.8 mm eight-layer stack, the aluminum-plugged blind vias, the immersion-gold finish, and the 100% flying-probe requirement without custom fixtures or array-count reductions. Panel utilization, handling rigidity, and downstream process compatibility were all improved relative to the original 4 mm all-around specification. With the files released, the job moved from CAM review into fabrication scheduling on the existing production line.
Frequently Asked Questions
Q1: Why did the original 4 mm process edges prevent panelization?
A1: The 4 mm border on all four sides produced a panel dimension that exceeded the usable working area once the 5x3 array and required routing clearances were applied. The adjusted 8 mm left/right rails and 2 mm top/bottom gaps yielded a practical 113.5 mm by 118 mm panel that fits standard equipment while still providing tooling and handling margin.
Q2: Why are process rails required on a 0.8 mm eight-layer board?
A2: Process rails supply the rigid border needed for automated handling, tooling-hole registration, and fiducial alignment. On a thin 0.8 mm stack they also limit flex during drilling, plating, and transport, reducing the chance of registration shift on the HDI blind-via layers.
Q3: What happens if a production number is requested but no character layer exists?
A3: Adding an undefined marking requires inventing placement, font, and location that were not supplied. Confirmation to omit the number avoids an incorrect or interfering legend and keeps the manufacturing files identical to the approved data set. Traceability can still be maintained through electronic lot tracking and the required test reports.
Q4: Why follow solder-mask openings that cross copper traces?
A4: When the customer documentation and the engineering confirmation both direct that the original openings be used, the mask geometry is retained exactly as supplied. This preserves design intent and eliminates a mask-layer edit. The resulting copper exposure is accepted as part of the approved fabrication package.
Q5: How does the optimized panelization improve manufacturing efficiency?
A5: The 113.5 mm by 118 mm panel keeps the full 5x3 array, fits standard working blanks, and provides rails wide enough for tooling holes and fiducials. Setup time, material waste, and fixture changes are reduced compared with an oversized or non-standard panel, while the 2 mm routing gaps support clean mechanical separation on the 0.8 mm board.
Q6: Can boards be manufactured without process rails or panelization?
A6: Single-board processing is possible but loses the throughput and handling advantages of a panel. For an 8-layer 0.8 mm order with blind vias and 100% flying-probe test, the confirmed 5x3 panel with optimized rails is the practical route to efficient fabrication and consistent registration.