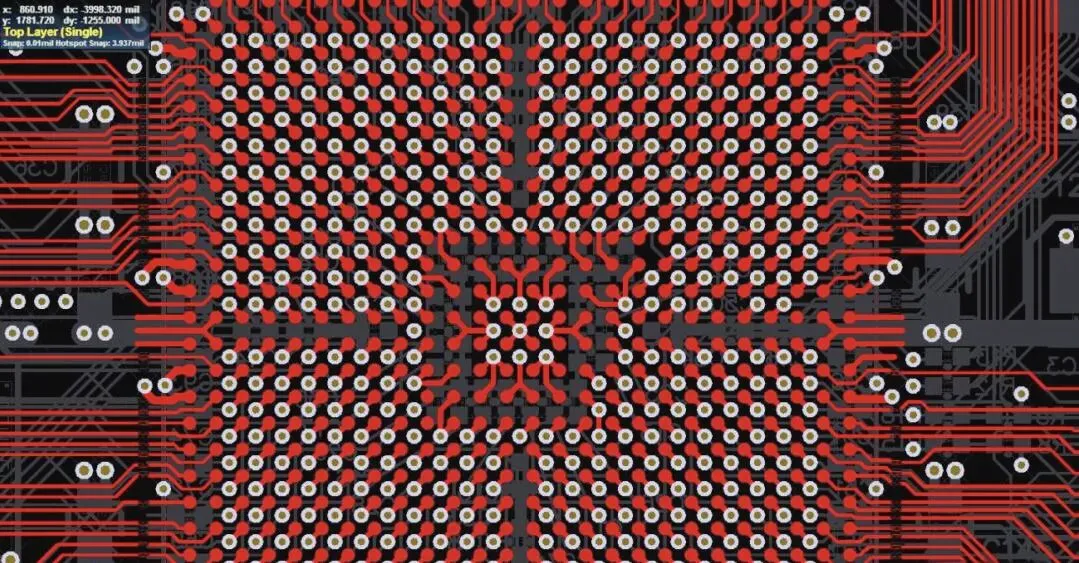
Solder paste printing is one of the most critical stages in surface mount technology (SMT) assembly. It determines how accurately solder paste is deposited onto PCB pads before component placement and reflow soldering. Even minor variations in paste volume, position, or shape can affect solder joint formation and lead to defects such as bridging, insufficient solder, and open connections.
As electronic products become smaller and more densely integrated, manufacturers face increasing challenges in maintaining consistent solder paste printing quality. Fine-pitch components, high-density PCB layouts, and miniaturized packages require more precise control over stencil design, solder paste properties, printing parameters, and inspection methods.
A reliable solder paste printing process therefore requires more than adjusting machine settings. It involves coordinated management of materials, equipment, environmental conditions, and process data. This guide examines the fundamentals of SMT solder paste printing, common printing defects, practical optimization methods, and SPI-based closed-loop quality control.
Fundamentals of the SMT Solder Paste Printing Process
Effective control starts with a shared understanding of key process elements. These span material selection, physical parameter settings, and environmental control. Each dimension interacts with the others, so consistent, quantified management is necessary to achieve stable print quality.
Alloy System Selection
Lead-free alloys have become the mainstream choice globally. Among them, SAC305 (Sn96.5Ag3.0Cu0.5) is widely adopted for its balanced performance. With a melting range of 217–219 °C, it requires higher reflow temperatures than traditional tin–lead systems (e.g., Sn63/Pb37 at 183 °C), but provides superior creep resistance and thermal cycling life. This makes it well suited to products with high reliability requirements, such as consumer electronics and communications equipment. Lower-cost alternatives (e.g., SAC105) exist, but typically offer inferior drop/shock performance. In many applications, SAC305 remains the preferred balance of performance and cost.
Solder Powder Particle Size Selection
Particle size must match stencil aperture size to ensure full aperture fill and clean release. A practical rule is that the minimum aperture should be able to accommodate approximately five solder powder particles across the limiting dimension. For general-pitch components (≥ 0.5 mm), Type 3 (25–45 μm) or Type 4 (20–38 μm) powder is typically suitable. For 0.3–0.4 mm fine-pitch QFP or CSP, favor Type 4 or Type 5 (15–25 μm). For 01005 passives and BGAs with ≤ 0.35 mm pitch, Type 5 or even Type 6 powder is strongly recommended, ideally paired with an electroformed stencil to improve release consistency.
Flux Type Selection
Flux chemistry directly affects print behavior and post-reflow cleanliness. No-clean (NC) and water-soluble (WS/OA) formulations now account for well over 90% of the market. Selection involves balancing activity against cleaning and reliability needs. Low- to medium-activity (L/M) fluxes are less corrosive and often acceptable without cleaning, making them attractive for high-reliability products. High-activity (H) fluxes offer stronger oxide removal but may leave corrosive residues, typically necessitating thorough cleaning. In practice, many manufacturers favor medium-activity no-clean pastes to achieve good wetting while minimizing cleaning cost and environmental burden.
Defining the Key Process Window
A stable environment underpins process consistency. A typical process window maintains 23 ± 3 °C and 40–60% RH. Outside this range, elevated humidity promotes moisture uptake in paste and increases solder balling risk; low humidity increases static, which can disturb placement of very small components. Equipment parameters should be set and maintained within this controlled environment, including squeegee pressure (30–50 N), print speed (10–50 mm/s), and stencil separation speed (0.5–3 mm/s).
Solder Powder Selection for Fine-Pitch Solder Paste Printing
Solder powder particle size affects how consistently paste passes through stencil apertures. If particles are too large relative to the aperture dimensions, incomplete filling and inconsistent paste release may occur.
Common solder powder classifications include Type 3, Type 4, Type 5, and Type 6. Smaller particles are generally used for finer apertures and more demanding printing applications.
For fine-pitch solder paste printing, engineers should consider the relationship between powder size, aperture dimensions, stencil thickness, and paste release characteristics.
This becomes particularly important when assembling fine-pitch QFPs, BGAs, CSPs, and miniaturized passive components. Selecting a finer powder may improve aperture filling, but it should also be evaluated against oxidation sensitivity, storage requirements, and material cost.
Key SMT Printing Parameters and Process Conditions
Stable SMT printing requires coordinated control of several machine and environmental parameters.
Squeegee pressure and speed: Pressure must be sufficient to maintain consistent contact between the solder paste squeegee and stencil without forcing excessive paste through the apertures. Printing speed affects paste rolling behavior and aperture filling.
Stencil separation speed: The separation process influences how effectively solder paste releases from stencil walls. Excessively fast or poorly controlled separation may contribute to incomplete deposits, smearing, or inconsistent paste shapes.
Stencil alignment: Accurate alignment ensures that solder paste is deposited onto the intended PCB pads. Fiducial recognition, board support, and mechanical positioning all influence registration accuracy.
Temperature and humidity: Environmental fluctuations can change solder paste rheology and affect printing consistency. Manufacturers should follow the solder paste supplier's recommended storage, conditioning, and operating conditions.
These parameters should be evaluated together. Changing one setting without considering the others may solve one printing problem while creating another.
Common Solder Paste Printing Defects and Root-Cause Analysis
Recurring defects in production are often the result of multi-factor interactions. A root-cause view reveals the systemic risks hidden beneath the symptoms and guides corrective actions that actually move yield.
Insufficient Solder / Missing Solder
Insufficient solder leads to underfilled joints and unreliable electrical connections, and in severe cases, open circuits. Common causes include clogged stencil apertures, excessively high squeegee pressure, too-fast separation, overly high paste viscosity, and inadequate paste warm-up. In one case, paste was used after only 2 hours of warm-up; condensation within the paste boiled off during preheat, tripling the incidence of solder balls and also causing localized insufficient solder due to abnormal rheology. Poor material handling can trigger multiple failure modes simultaneously.

Excess Solder / Bridging
Excess solder and bridging create shorts between adjacent pads—at best affecting signal integrity, at worst damaging the PCB. Causes include an overly thick stencil, too-low squeegee pressure, too-slow separation, oversized apertures, and high ambient humidity. When shop-floor humidity remains above 60% RH, bridging rates can increase significantly (e.g., by a factor of 2.8 in observed cases). This highlights the leverage of environmental control: small drifts can magnify into serious quality issues.
Offset / Misregistration
Offset describes a printed paste pattern that is shifted from the pad centers and directly impacts placement accuracy. Root causes are alignment failures such as fiducial (MARK) recognition errors, worn or loose tooling, or insufficient stencil tension (e.g., below 35 N/cm2). In one monthly SMT report, print offset accounted for 2.97% of all defects—a persistent issue that often indicates shortcomings in equipment maintenance and calibration.
Peaking / Tailing
Peaking appears as icicle-like spikes at the trailing edge of the paste deposit and can cause shorts or weak joints. It is typically driven by too-fast separation (snap-off), rough stencil sidewalls, or an improper squeegee angle. This defect is highly sensitive to the separation process; small parameter mismatches can quickly produce a large number of rejects.
Solder Balls / Spattering
Solder balls are small spheres that appear around the joint after reflow and may create latent shorting risks. The mechanisms are multifactorial, including excessive temperature ramp rate (quantities increase sharply above about 3 °C/s), contamination on the stencil underside, moisture in the paste, and low metal loading. Ramp rate is especially critical: if the solvent system does not outgas gradually, it can spatter during peak zones and eject fine solder particles that later reflow into solder balls.

Solder Paste Printing Optimization and Closed-Loop Process Control
Addressing these defects requires a systemic optimization strategy that integrates precise parameter settings, closed-loop feedback, and disciplined material control into a single framework.
Guidelines for Fine-Tuning Parameters
Parameter settings must be tailored to specific component types. For fine-pitch QFP, set squeegee pressure to 2.5–3 kg to avoid paste squeeze-out from excessive pressure. For BGAs and large pads, increase pressure to 4–5 kg to ensure deep apertures are fully filled. Control separation speed by component class: for ultra-small components such as 01005, use 3–5 mm/s; in general cases, 5–8 mm/s balances release completeness and throughput. Squeegee speed, attack angle, and stencil separation should be co-optimized rather than tuned in isolation.
Stencil Design and Maintenance Standards
The stencil is the most critical tooling element for print quality. Design targets should include an area ratio greater than 0.66 and an aspect ratio greater than 1.5 to ensure effective paste release. New stencils should favor electroformed (e.g., FG) construction with nano-coatings to reduce wall friction, and initial frame tension should be at least 40 N/cm2 to maintain registration. In routine maintenance, verify stencil flatness (≤ 15 μm) and correct deformation promptly to prevent local gap variation that causes thickness non-uniformity. A robust underside cleaning protocol and periodic aperture inspection help maintain stable transfer efficiency.
Material and Environmental Control
Solder paste handling is foundational to process stability. Refrigerate paste at 0–10 °C and allow at least 4 hours of natural warm-up before opening. Do not open containers before warm-up to avoid condensation ingress. After opening, use within 24 hours; do not mix returned paste into fresh containers to avoid contamination and loss of activity. Implement real-time environmental monitoring for temperature and humidity with alarm thresholds, and enforce immediate corrective actions when limits are exceeded.
Build an SPI-Based Closed-Loop Control System
The most impactful step is to center control around solder paste inspection (SPI) with automated feedback. A well-implemented system can provide:
- Real-time feedback: When SPI detects thickness non-uniformity, automatically increase print pressure; when volume is low, reduce squeegee speed to lengthen aperture fill time.
- Collaborative linkage: Synchronize offset data from SPI to the pick and place system to adjust placement coordinates and compensate for upstream print misalignment.
- CPK monitoring: Continuously compute the process capability index (CPK). When CPK < 1.0, trigger alerts and initiate targeted corrective actions before defects escalate.
In a representative consumer electronics line, introducing this closed-loop reduced downtime by 40% and raised first-pass yield from 85% to 98%, demonstrating the potential of data-driven optimization to deliver measurable improvements.
The Future of SMT Printing: Advanced Solder Paste Deposition Technologies
As electronic assemblies become more compact, SMT printing technology continues to evolve toward greater precision, automation, and process visibility.
Several developments are shaping the future of SMT printing.
Advanced stencil technologies: Improved aperture manufacturing, surface treatments, and customized stencil structures help address the challenges of miniaturized components and high-density PCB layouts.
Automated process monitoring: Modern inspection systems can collect printing data across production runs, allowing engineers to identify variations before they result in widespread defects.
Closed-loop manufacturing: Integration between SPI equipment, stencil printers, and manufacturing execution systems supports faster feedback and more consistent process control.
Alternative deposition methods: For specialized applications, jet dispensing and other direct-deposition technologies may complement conventional stencil printing. These approaches can be useful where conventional stencil-based processes face limitations in localized or highly customized solder paste deposition.
The adoption of advanced solder paste deposition technology should be driven by application requirements, production volume, component geometry, and process economics rather than technology trends alone.
Conclusion
Solder paste printing is a foundational process in SMT assembly, and its quality directly affects downstream soldering performance and manufacturing yield.
Consistent results depend on selecting suitable solder paste, optimizing stencil geometry, controlling printing parameters, maintaining stable environmental conditions, and using inspection data to identify process variations.
For high-density and fine-pitch PCB assemblies, these factors become even more important. Combining proper process engineering with SPI-based quality control allows manufacturers to reduce printing defects and improve assembly consistency.
FAQ
Q1: What are the best solder pastes for high-reliability electronics assembly?
A1: The best solder paste depends on the alloy requirements, component pitch, operating environment, and reliability standards of the finished product. SAC305 is a widely used lead-free option, but engineers should also evaluate flux activity, powder particle size, residue behavior, and compatibility with the reflow profile. Automotive, industrial, and medical electronics may require additional qualification and reliability testing.
Q2: How can solder paste printing quality be controlled in SMT manufacturing?
A2: Solder paste printing quality can be controlled through appropriate stencil design, stable machine parameters, correct paste handling, and regular inspection. SPI systems help monitor paste volume, height, area, and alignment. Reviewing inspection trends enables engineers to identify recurring problems and make targeted process adjustments.
Q3: What causes insufficient solder paste during PCB assembly?
A3: Insufficient solder paste can result from clogged stencil apertures, poor paste release, unsuitable aperture dimensions, incorrect printing parameters, or improperly conditioned solder paste. Engineers should inspect the stencil, verify material condition, and review SPI measurements to identify the underlying cause.
Q4: Why is fine-pitch solder paste printing more challenging?
A4: Fine-pitch solder paste printing involves smaller pad dimensions and tighter spacing between adjacent connections. This reduces the available process margin and increases sensitivity to stencil aperture geometry, solder powder size, alignment, and paste volume. Accurate stencil design and consistent inspection are essential for reliable results.
Q5: What is the difference between conventional SMT printing and advanced solder paste deposition?
A5: Conventional SMT printing typically uses a stencil and squeegee to transfer solder paste onto PCB pads simultaneously. Advanced deposition methods may use customized stencil structures, automated feedback, or direct dispensing technologies to address specialized printing requirements. The appropriate method depends on PCB design, production volume, and required deposition precision.