Hardware designers are often asked to meet the performance target and then reduce cost further. In high-speed board design, impedance matching cannot be skipped, but multilayer boards are expensive, and a 2-layer board appears unable to support controlled impedance. That conflict raises a direct question: is there a workable path?
In high-speed board design, impedance matching is a required task. On boards with four or more layers, dedicated reference planes make impedance control relatively straightforward. On a lower-cost 2-layer board, many engineers run into trouble. There is no dedicated reference layer, and conventional stackup-based calculations do not apply. That does not mean a 2-layer board is incompatible with impedance matching.
A 2-layer board can still implement impedance matching if the return path is designed correctly. The goal is to balance performance and cost.

1. Where Impedance Matching Is Difficult on a 2-Layer Board
The purpose of impedance matching is to deliver the signal to its destination with reduced reflection and loss, and to protect signal quality. Multilayer boards are easier to design because a reference plane provides a defined basis for impedance calculation.
A 2-layer board lacks that reference plane, which leads to three problems that stop many designs:
- There is no dedicated reference layer, so the signal has no clear return reference.
- Conventional board-thickness and trace-width calculation methods no longer apply.
- Small layout errors can distort the signal and make performance difficult to guarantee.

2. The Key: Provide a Continuous Return Path with Ground Guarding
A 2-layer board can support impedance matching when the design follows the correct principle. Practical work shows that the critical requirement is a complete, uninterrupted current return path for the signal.
In layout terms, that is ground guarding. One rule is fixed: the ground traces used for guarding must be continuous and must not be broken. From a modeling standpoint, this structure is a coplanar impedance geometry. For a 2-layer board, it is the only practical approach described here for implementing impedance matching.


3. SI9000 Parameters for 50 Ω, 90 Ω, and 100 Ω
Theory alone is not enough. The industry impedance calculator SI9000 was used to produce three commonly used targets: 50 Ω single-ended, 90 Ω differential, and 100 Ω differential. Each set includes the corresponding calculation screenshot and can be used as a starting design reference.
3.1 50 Ω Single-Ended
Key parameters: lower trace width 23.0000 mil, upper trace width 22.5000 mil, ground-trace spacing 5.0000 mil, substrate height 60.0000 mil. SI9000 result: 50.21 Ω. The error is small enough for direct use in this case.

3.2 90 Ω Differential Pair
Key parameters: lower trace width 9.3000 mil, upper trace width 8.8000 mil, pair spacing 5.0000 mil, ground-trace spacing 5.0000 mil. SI9000 result: 89.96 Ω, close to the target and stable in this calculation.

3.3 100 Ω Differential Pair
Key parameters: lower trace width 6.2000 mil, upper trace width 5.7000 mil, pair spacing 5.0000 mil, ground-trace spacing 5.0000 mil. SI9000 result: 99.84 Ω. The accuracy is high and is suitable for designs with tighter signal requirements.

4. Production Example: Telecom Set-Top Box
A production example is more useful than theory alone. In one telecom set-top box teardown, the product used a 2-layer board for cost reduction and still implemented impedance matching.
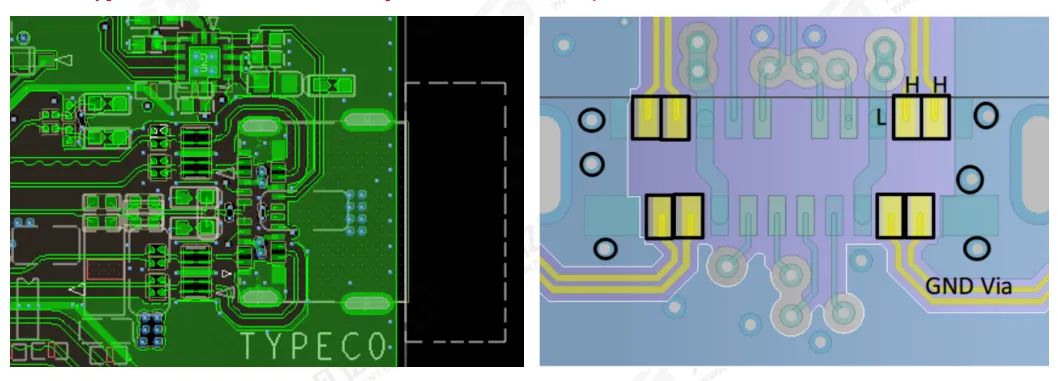
The board can be identified as 2-layer from the teardown photos: when light is applied from the back, it passes through the PCB. A multilayer board would not transmit light at that level. The main layout method is the ground-guarding approach described above, applied in three ways:
- Single-sided ground guarding: a continuous ground trace is placed on one side of the signal line to keep the return path continuous.
- Increased spacing: enough distance is left between two signal lines to reduce interference.
- Paired ground guarding: an independent ground trace is placed between every two signal lines to further improve signal stability.
The design makes some compromise in signal quality, but it meets the set-top box application requirements. Cost is more than 30% lower than a multilayer board.

5. Practical Constraint: The 23 mil Width Required for 50 Ω
One limitation is hidden in the parameters above. The 90 Ω and 100 Ω widths are still workable, but the 50 Ω case requires a 23 mil trace width. That width is rarely practical in real PCB routing, especially for dense single-ended buses such as DDR, where a 23 mil width on every net cannot be placed.
A common industry compromise when cost comes first is to relax the impedance target:
- Relax the 50 Ω target to 60–70 Ω before calculating. This keeps basic performance while reducing width and easing routing.
- Give routing feasibility priority. Signal quality only needs to meet the product requirement. Extreme impedance accuracy is not required if the nets cannot be routed.
- Follow production needs. Use the set-top box combination of single-sided ground guarding, increased spacing, and paired ground guarding to balance cost and signal quality.
6. Summary: Cost Reduction Depends on the Return-Path Details
Impedance matching on a 2-layer board comes down to one task: provide a complete return path with continuous ground guarding, then adjust the parameters for the actual application. It is not the best electrical solution, but it is a cost-effective solution. Finding the balance between cost and performance is the core of the design.
Key points:
- Define the requirement first. Set the impedance target from the product use case. Do not pursue high precision by default.
- Choose the stackup that fits the need. Multilayer boards are easier, but they cost more. A 2-layer board can meet the requirement if the method is applied correctly.
- Control the details. Continuous ground traces and reasonable spacing determine the impedance-matching result.
- Balance cost and performance. Avoid overdesign. Meeting the core requirement is the right design target.

In hardware design, cost control and engineering method are not opposites. If a 2-layer board can do the job, a multilayer stackup is not required. That is both a technical choice and a cost decision.