A PCB hole-tolerance issue usually reaches CAM when the hole chart already defines a finished size and tolerance, but the shop reports that the specified window is difficult to hold on the released opening. The files still treat the feature as a drilled hole or slot, while production is asking to widen the tolerance, change the forming method, or both.
Three recent packages showed the same gap in different ways. One ZIP released three slots and three large holes as drill tools; the shop could not drill the named lengths or diameters on that job and proposed routing those six openings during forming with the tolerance opened to ±0.1 mm. A second drawing marked plated holes whose tolerance was too tight to hold, while the plated slots on the same sheet carried a similar issue. A third drawing marked NPTH tools and reported that the specified diameter window was too tight to control in production. These three EQs are examples from recent jobs, not a complete list of hole-tolerance questions.
| What we saw in the files | Where the files disagree | What the EQ asked |
|---|---|---|
| Three slots and three large holes released as drilled openings | Shop cannot drill the named length or diameter on this job | Accept ±0.1 mm and route those six tools at forming? |
| Arrow-marked plated holes and plated slots on the same drawing | Written hole tolerance and slot tolerance cannot be held on those tools | Confirm the plated band, or write a different size, band, or forming method |
| Arrow-marked NPTH tools with a tight diameter band | Shop states the NPTH diameter is too tight to control in production | Confirm the released NPTH band, a looser written band, or routing on those hits |
PCB Hole Tolerance and Slots in the Released Package
Finished PCB hole size, slot size, and the written band are already in the ZIP. They appear on the hole chart, the drill drawing, or a fabrication note. NC drill and outer copper show the hits and any slot outline. CAM is reading those calls rather than assigning a new window to a tool that never carried one.
The files can describe the same tool differently. A chart row may list one diameter while the Excellon tool is another. A note may call a slot plated while the copper at that outline has no land. In that case the starting point is still the row that named the tool, not a factory default.
A slot is a length-and-width opening. If the chart marks it plated, copper and a barrel still belong to that tool. If the chart marks it NPTH, they do not. Large holes sit in the same review as the slots because both are finished openings with a written band. Size on its own does not convert a drill tool into a routed outline cut.
PTH or NPTH on that row is the plated attribute for the tool. This article leaves the plated-flag review in its own cluster. The flag matters here only because a tight plated call and a tight NPTH call close differently once copper is considered. Routing a plated slot as an NPTH profile cut changes both the forming method and the plating, so both belong on the close line.

PCB Drill Hole Tolerance Versus Slot Size on the Hole Chart
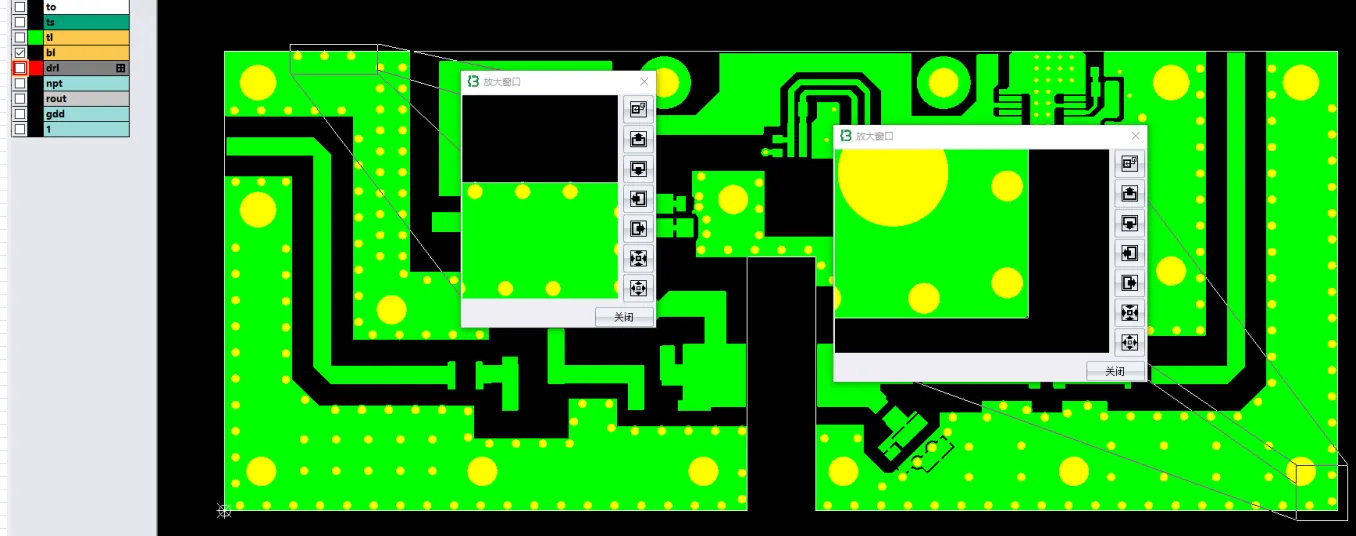
Overlaying the hole chart, NC drill data, and copper at the same coordinates can show the finished size on the row, which tools are slots and which are round, plated or NPTH on that row, whether copper sits on a plated hole or plated slot, and where the hit or the slot ends sit against the outline.
The overlay establishes the released geometry and the relationship between the opening and nearby copper. Whether the specified tolerance can be held, whether routing is an acceptable substitute, and whether the hardware still fits after a tolerance change require manufacturing or design confirmation.
Drill hole tolerance is a finished-size band. It is separate from plating thickness, annular ring, and press-fit class. A large plated hole with a tight window remains a hole-tolerance question in this review; the diameter alone does not move the tool into a press-fit discussion.
For a slot, length and width come from the slot outline or the chained hits, then from the tolerance line that points at them. For the plated EQ, copper or a barrel call on those tools is part of the evidence. For the NPTH EQ, the chart still needs to read non-plated even if copper is nearby. Nearby copper does not change the NPTH flag. Disagreement between chart and copper on plating is a separate PTH versus NPTH close.
| Source in the package | What it can show | What it still leaves open |
|---|---|---|
| Hole chart / drill drawing / note | Named diameter or slot length and width, written band, plated or NPTH on that row, how many hits | Whether the shop can hold that band on this tool, or whether ±0.1 mm still fits the pin |
| NC drill vs copper at the same XY | Round hit versus slot outline, copper or no copper on a plated call, isolated flash next to an NPTH row | Whether a plated slot may become an NPTH routed opening |
| Board outline vs slot ends or large-hole wall | Where the opening sits against the profile, and whether a route-at-forming path would join the outline cut | Slot-end radius and edge quality after routing |
| Factory EQ line | Which tools the shop named, the proposed ±0.1 mm, and route-at-forming on the three slots and three large holes | Connector, standoff, or alignment fit after the band or the method changes |
PCB Slots and Large Holes When Forming Changes from Drill to Route
The first EQ names three slots and three large holes. Those six tools left the package as drilled openings. The shop could not drill them as drawn and asked to route the openings at forming and open the hole tolerance to ±0.1 mm. The request applies to those six tools. The remainder of the drill list does not inherit that pair of changes.
Two requests share the same note. The tools are too long or too large to drill on this job, and the proposed close is ±0.1 mm plus route the opening during forming. Routing at forming is the outline cut rather than a second drill pass or a stamp-hole row. Slot ends change with the method: a drilled slot finishes in the bit radius, a routed slot follows the cutter used on the profile. If any of the six tools were plated, the barrel may no longer be present after the method changes, so that change needs to be named. If they were already NPTH, the remaining questions are the band and the forming method.

Three slots and three large holes are too long or too large in diameter
This review does not attach a maximum drillable diameter or slot length to the job. The shop statement on these six tools is the evidence in the package. ±0.1 mm remains the proposal on that EQ. It is not treated as a house standard, and it is not applied to unmarked holes in the same list.
Before the note is sent, the three slots and three large holes are identified by tool and XY, together with the released length or diameter, the written tolerance, and plated or NPTH on those rows. Accept or reject then applies to those six tools: band to ±0.1 mm, and route the opening during forming instead of drill.
Plated Slots When the PCB Hole Tolerance Is Tight
The second EQ marks plated holes whose plated hole tolerance the shop cannot hold. The plated slots on the same sheet carry a slot tolerance the shop cannot hold either. The tools remain plated. Copper and a barrel are still present. A wider finished size does not remove plating from the tool and does not decide whether the pin still functions.
A plated slot is generally harder to hold than a round plated hole of similar width, because length, wander, and both slot ends sit inside the same written band. The drawing treats the plated holes and the slots as one confirmation. That grouping is useful on the sheet; it is not, by itself, a reason to convert the slots to NPTH routed openings without a written line.
CAM can show the marked tools, the chart tolerance, and copper at those hits. Converting a plated slot to an NPTH routed slot is a file change, not an overlay result. A tight plated tolerance is also a different question from whether the hole should have been PTH. If the chart already says plated, the flag is already answered. The object of this EQ is the band.

Exact slot tolerances
The close on this sheet is keep the plated band, accept a written looser band on those tools only, or send a new file with a different size, plating call, or slot forming method. The barrel is left as released unless the close also changes plating. The EQ is not closed against an IPC class table. The customer window remains until a new chart row replaces it.
NPTH Drill Hole Tolerance on the Named Diameters
The third EQ marks NPTH holes and reports that the diameter tolerance is too tight to control in production. With plating out of the comparison, what remains is finished diameter against a mechanical drill or a routed opening. There is no barrel to average the cut.
That is still a NPTH hole diameter tolerance question on named NPTH tools. It is not a request to add pads or convert the holes to PTH. Nearby copper does not change the NPTH flag. If the chart and the copper disagree on plating, that close belongs with the PTH versus NPTH review.

The NPTH hole tolerance at the arrows is too tight for production control
"Hard to control" is a statement on this job rather than a published NPTH capability chart. If these NPTH holes are the same three large holes from the first EQ, they can share one close line. If they are a different marked set, they stay separate so that a ±0.1 mm and route accept on the long slots does not rewrite every NPTH tool on the board.
A looser NPTH band is often refused because of fit: a standoff, a pin, or an alignment feature. Gerber does not show that fit. CAM can measure the released diameter and the written band. Whether the hardware still seats after the window changes is the confirmation the note is requesting.
Keep the Released PCB Hole Tolerance or Confirm Routing and ±0.1 mm
Each finding is closed on its own written line. The drill list is left as released until that line arrives.
If the release is kept, the named sizes and tolerances remain. The customer either accepts the process consequence named in the EQ or supplies another forming method that still meets the original band. CAM does not supply that method on its own.
If the factory line is accepted, it applies only where it was asked: ±0.1 mm on the tools named in that EQ, and route-at-forming only on the three slots and three large holes when that accept is written. Other drill tools do not inherit the band. A plated-slot accept that only widens the window still leaves the barrel. Routing a plated slot or plated large hole as an NPTH profile cut changes both method and plating, and both belong on the close line.
If the files change, the customer sends a new chart: new diameter or slot size, new tolerance line, plated or NPTH restated, and updated copper if a plated slot becomes a routed NPTH opening. After that file arrives, copper is reviewed again on any plated tool whose finished size or forming method changed. ±0.1 mm is not copied onto unmarked holes.
| Finding | Keep the release | Accept the factory line | Change the files |
|---|---|---|---|
| Three slots and three large holes, too long or too large to drill | Keep the six tools as drilled openings at the released size and band | ±0.1 mm and route the opening during forming on those six tools only | New chart row: new size, new band, plated or NPTH restated; copper updated if a plated opening becomes an NPTH profile cut |
| Arrow-marked plated holes and plated slots, tight band | Keep the plated finished-size band; barrel and lands stay | Written looser band on the marked plated tools only; plating stays unless the close also drops it | New diameter or slot size, new band, or a forming-method change that names plating |
| Arrow-marked NPTH diameters, tight band | Keep the NPTH diameter and band on the named tools | Written looser band, or routing if that method is offered on those hits | New NPTH size or band in a revised chart; pads and a PTH change remain a separate close |
Until one of those lines is written, the released PCB hole tolerance, the released slot geometry, and the released plated or NPTH flag remain as drawn. The EQ is a request for confirmation, not a revised manufacturing instruction.
FAQ
Q1: What is the standard tolerance for PCB holes?
A1: This review does not publish a single standard number. PCB hole tolerance is the finished-size band written on the hole chart, the drill drawing, or the fabrication note. If the package never wrote a band, CAM does not insert one. ±0.1 mm in the first EQ is the shop proposal on those named tools. It is not treated as a house standard or as a default for the rest of the drill list.
Q2: What is the difference between drill size and finished hole size?
A2: The chart row is calling the finished opening after the hole is made. Drill hole tolerance is that same finished-size band. It is separate from plating thickness and annular ring. On a plated tool the finished diameter still includes the barrel. On an NPTH tool it does not.
Q3: What is a plated slot on a PCB?
A3: A slot is a length-and-width opening. A plated slot still has copper and a barrel; an NPTH slot does not. The plated flag comes from the chart row, not from the opening being long. If that plated slot later routes as an outline cut, the barrel may no longer be present. That is a second decision on the close line.
Q4: Can PCB slots be drilled, or do they have to be routed?
A4: Either method can be the released instruction. In the first EQ the three slots and three large holes were released as drilled openings. The shop could not drill the named length or diameter and asked to form them during outline routing, with the band opened to ±0.1 mm. That reason belongs to those six tools. It is not a published maximum slot length, and the rest of the drill list does not inherit the method change.
Q5: What is NPTH hole tolerance?
A5: It is the same finished-size band, applied to tools the chart already marks non-plated. The third EQ marks those diameters and reports that production cannot hold the written window. Nearby copper does not turn the tool into PTH. Adding pads or converting the holes to plated through holes is a different close.
Q6: Why is plated-slot tolerance harder to hold than a round plated hole?
A6: Length, wander, and both slot ends sit inside one written band. The second EQ treats the marked plated holes and the plated slots as one confirmation for that reason. The confirmation is still the band. It does not drop plating on the slots, and it does not rewrite unmarked plated tools on the same sheet.
Q7: What DFM checks apply to PCB holes and slots?
A7: On these jobs the practical DFM question is whether the released finished size and forming method can be run on the named tools. It is not whether the board passes a generic hole-and-slot checklist. This review does not publish a capability table. The evidence is the chart row, the overlay at the hit, and the shop statement on those tools.
Q8: Who decides if the factory can open the tolerance to ±0.1 mm?
A8: The customer, in a written close that names the tools, the band, the forming method, and whether plating stays. CAM records the released size and tolerance, the overlay at each named hit, and the factory line. Large holes are not all opened to ±0.1 mm, unmarked slots are not all routed at forming, and a plated barrel is not removed only because the window was tight. Until that line is written, the released PCB hole tolerance and the released slot geometry remain as drawn.