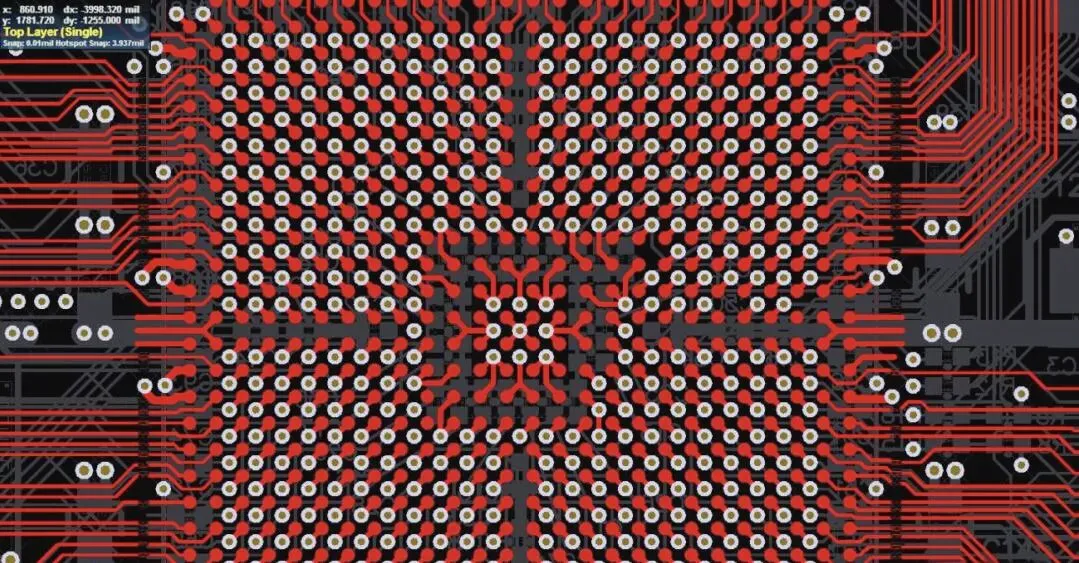
PBGA (plastic ball grid array) is a package family whose defining characteristic is the use of an array of solder balls to make contact with the substrate, typically a printed circuit board. Compared with packages that use other lead configurations, such as single-row, dual in-line, or quad packages, this ball-array approach delivers a clear advantage: a considerably higher pin density within the same footprint. Inside the package, the die is connected to the substrate either through wire bonding or through flip-chip technology, and the integrated circuit itself is encapsulated in a molding compound.

Figure 1 | Schematic diagram of a PBGA device
Once a PBGA device has been assembled onto a PCB and a defect is discovered, the board must be reworked: the faulty device is removed and a known-good device is installed in its place. Before removal, the device has to be heated until the solder joints liquefy, so that it can be lifted from the circuit board. This article walks through each stage of that procedure, from board preparation and device removal through pad cleaning, solder paste application, alignment, placement, and final inspection, with attention to the process controls and equipment settings that determine whether the rework produces a reliable joint or introduces new damage.
Highlights:
- Bake the PCB assembly before rework to drive off residual moisture; otherwise the popcorn effect can damage the device during reflow.
- Keep rework temperatures below the peak temperature stated on the moisture sensitivity level (MSL) label, hold the peak above liquidus for less than 60 seconds, and calibrate the profile for every new device, solder composition, and board configuration.
- Placement accuracy must keep the offset below 50% of the PCB pad width, because misalignment beyond that point can cause solder bridging and electrical shorts.
Reworking a PBGA Device
Removing a device and delaminating it from the board are the first steps of any rework, and they are also the steps most likely to introduce mechanical stress into the PBGA and the PCB. The faulty device must be removed carefully to avoid damaging the board, the neighboring components, and the device itself. The last point matters especially when the user intends to perform failure analysis on the removed part, since a device that has been roughly handled or overheated can no longer be trusted as evidence of the original failure.
Excessive stress on a PBGA device, applied for example by heating it above its rated peak temperature or by exposing it to elevated temperature for too long, can cause package delamination or external physical damage. Delamination caused by improper removal makes it harder to identify the true failure mechanism, so careful removal is a prerequisite for effective failure analysis.

Figure 2 | Delamination between the substrate and molding compound of a PBGA device caused by overheating (observed by scanning acoustic microscopy)

Figure 3 | Low-magnification image of cracks on a PBGA caused by overheating (side view)
The standard rework sequence runs as follows:
- Prepare the board.
- Remove the device.
- Clean the PCB pads.
- Apply solder paste.
- Align and place the device.
- Secure the device.
- Inspect.
Step 1: Preparing the Board
Before SMD rework begins, the PCB assembly should be baked dry to eliminate residual moisture. If that moisture is not removed, it can damage the device during reflow through the popcorn effect. Bake the assembly at 125 °C for at least 4 hours, provided these conditions do not exceed the ratings of other components on the board. If they do exceed those ratings, use the alternative bake conditions specified in the joint industry standard IPC/JEDEC J-STD-033.
Step 2: Removing the Device
A range of tools can be used for device removal. In principle, the device is heated until the solder reflows and is then lifted away mechanically while the solder is still liquid. A programmable hot-air rework system provides controlled temperature and time settings, which makes it the more repeatable choice.
Rework should follow the same temperature profile that was used to assemble the device. The rework temperature must not exceed the peak temperature stated on the moisture sensitivity level (MSL) label. Heating time may be shortened, for example in the liquefaction zone, as long as the solder fully reflows; the time spent at peak temperature in the solder reflow zone should be less than 60 seconds. The vacuum pressure of the pick-up tool should be less than 0.5 kg/cm2 to prevent the device from being dislodged before full reflow is reached and to avoid lifting pads off the board. Devices removed from a PCB must not be reused.
Rework temperature must be controlled to avoid damaging both the PBGA device and the PCB. Because of differences in thermal mass, a PBGA may heat up faster than leadframe-based packages such as standard-outline integrated circuits (SOIC) and leadframe chip scale packages (LFCSP). Covering the area around the device with heat-resistant tape provides additional protection. Heating the underside of the PCB is also recommended, since it reduces the temperature difference between the two sides of the board and minimizes board warpage.
Temperature profiles should be calibrated when the rework tool settings are defined. This calibration is particularly important the first time a specific device is reworked. PBGA devices with different body sizes, solder compositions, or different PCB materials, configurations, sizes, and thicknesses also need to be calibrated, because they may have different thermal mass values.

Figure 4 | Simplified flowchart for device removal evaluation
Calibration must include monitoring of temperature, time, and the other tool settings of the equipment. Thermocouples should be attached to different parts of the board assembly, such as the top of the PBGA device and the top of the PCB. The time and temperature profile data are then analyzed to derive effective device removal parameters from the evaluation.

Figure 5 | Schematic diagram of the calibration setup for device removal
Step 3: Cleaning the PCB Pads
After the PBGA device is removed, the pads on the PCB carry excess solder, which must be cleaned up before the replacement PBGA is installed. Pad cleaning is a two-part operation.
Desoldering
Use desoldering braid and a blade-type soldering iron to remove excess solder from the pads. The width of the selected blade should match the largest width occupied by the device. The blade temperature must be low enough to avoid damaging the circuit board. Flux can be applied to the pads first, after which the braid and iron are used to remove the excess solder.

Figure 6 | Removing solder from PCB pads
Cleaning
Clean the rework area with a cleaning agent and wipe it dry with a lint-free cloth. The cleaning agent selected depends on the type of solder paste used in the original assembly.
Step 4: Applying Solder Paste
Solder paste should be applied before the replacement PBGA device is mounted on the board. The purpose is to replace the paste applied during the original board assembly and thereby ensure the reliability of the PBGA solder joints. The volume of paste applied to each solder ball must be consistent, otherwise coplanarity problems can arise when the PBGA is placed on the board.
A stencil can be used to apply paste to the PCB pads. Stencil alignment accuracy is the key to keeping the reflow soldering process uniform. Use the same PBGA aperture geometry and stencil thickness as the board assembly process. Trapezoidal apertures ensure uniform paste release and reduce smearing.

Figure 7 | Stencil aperture geometry (A is longer than B)
In some cases, applying paste uniformly and precisely to the PCB pads with a stencil may not be practical, particularly on boards with high device density or tight geometric constraints. In those situations, consider applying the paste to the solder balls on the underside of the device instead. This can be done by printing paste onto the top of the balls with a stencil, or by dispensing paste onto all of the balls. A purpose-designed fixture and/or the rework equipment can be used to accomplish this.

Figure 8 | Printing solder paste onto solder balls with a solder paste stencil

Figure 9 | Dispensing solder paste onto solder balls
Step 5: Device Alignment and Placement
Accurate placement of the device on the board is essential. Placement equipment with a split-beam optical system assists in aligning the PBGA with the circuit board. Such an imaging system superimposes the mirror image of the PBGA solder balls on the mirror image of the PCB pads. The placement machine must give the user the ability to make fine adjustments along the x and y axes, including rotation.

Figure 10 | Aligning the PCB and device using a split-beam optical system
Placement accuracy depends on the equipment or process used. Although PBGA packages tend to self-align during reflow soldering, make sure the placement offset is less than 50% of the PCB pad width. If the alignment error is too large, solder bridging can cause electrical shorts.
Step 6: Securing the Device
Because all reflow parameters have already been optimized, use the thermal profile established during the original assembly process.
Step 7: Inspection
After reflow, inspect the assembled PBGA for defects such as misalignment or damage. Use X-ray inspection to check for problems such as solder bridging and solder balls. If necessary, perform electrical verification tests to confirm that the device functions correctly.
Related Reading:
Eight Layout Considerations for Differential Filters on PCBs
Improving PCB Immunity to Power Supply Variations in Converter Systems
PCB Layout for Accurate Temperature Measurement: PCB vs Ambient
Best Grounding Practices for Data Converters: Return Paths and Error Voltage
High-Temperature IC Packaging: Die Attach, Wire Bond, Solder and PCB
isoPower Radiated Emissions: Dense PCB Layout Guide
Buck Regulator PCB Layout and Grounding Guide for Low Noise
PCB Thermal Design: Junction Temperature and Power Dissipation